Plywood vs Steel Formwork: Cost, Reuse, Finish, and When Each Wins
Plywood vs steel formwork compared on cost per pour, reuse, finish, weight and labour, with one comparison table and clear cases for when film-faced plywood or HDO beats steel and when steel wins.
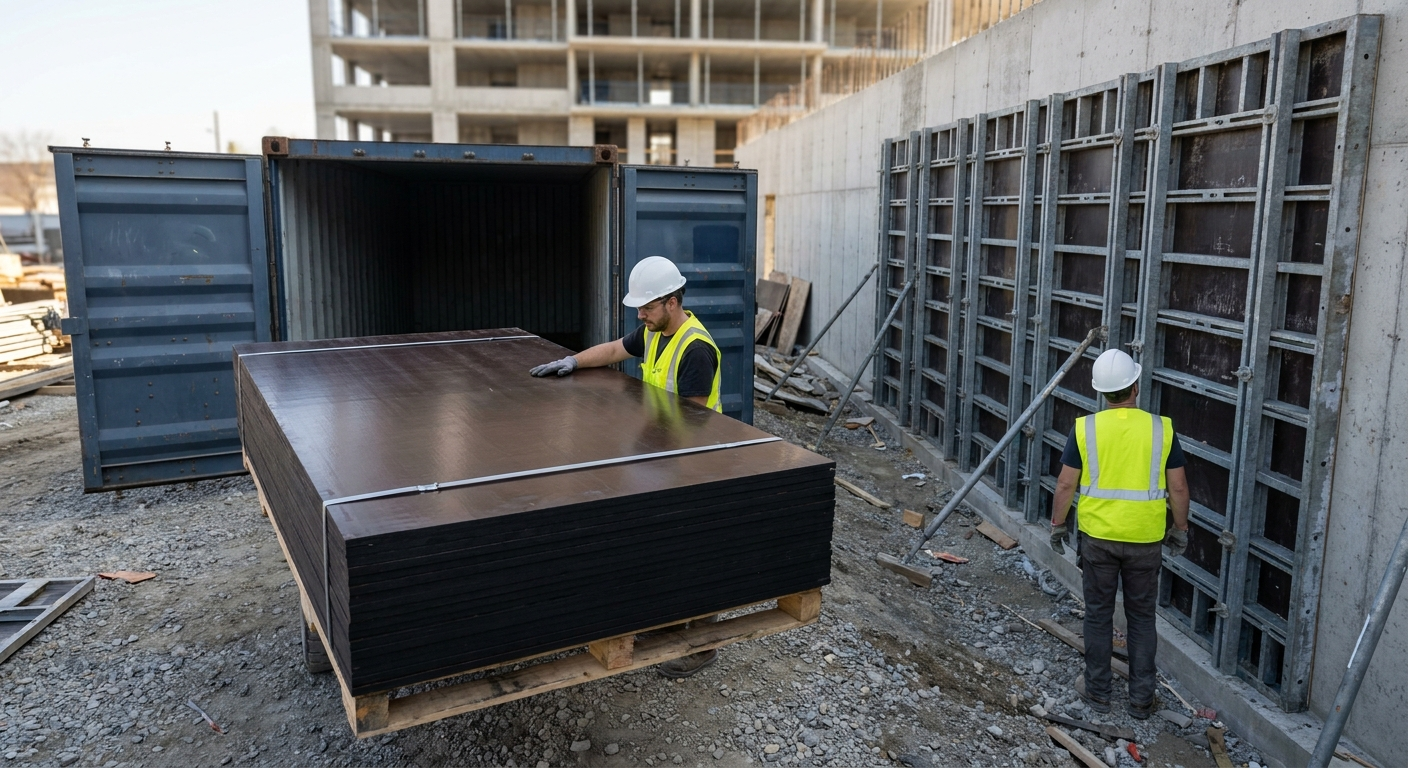
Short answer: on most building jobs, plywood-faced forms come out cheaper per pour than steel. That's true when each form sees a moderate number of pours, when the shapes keep changing, and when the crew sets panels by hand. Steel pays for itself only when one section repeats at very high volume and there's enough of the programme left to spread its cost over. And a good share of what gets sold as steel formwork is really a steel frame with a plywood face bolted in, so the two end up on the same site more often than the argument suggests.
We make film-faced formwork plywood in Vietnam, have done since 1992, and ship roughly 5,000 containers a year to 55+ countries. So yes, we lean toward panels. We've still tried to give steel a fair hearing here. A contractor who puts panels on a job that really needed a steel fleet loses far more than any saving on sheet price, and we'd rather not be the reason.
Two systems that often share one form
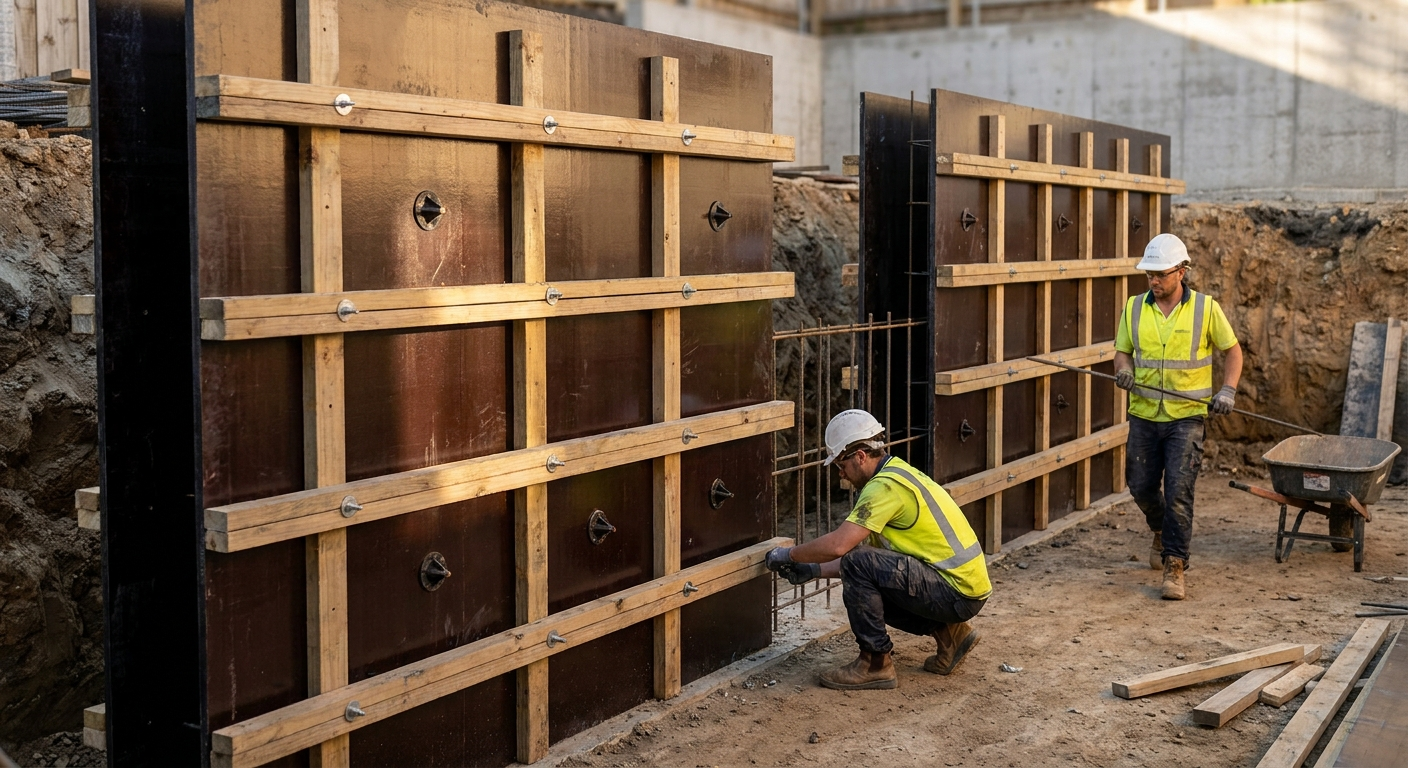
Start with the plywood side. It's a sheet, 18 mm in most cases, fixed to a frame of timber, aluminium or steel, or simply laid over timber beams on a slab deck. Concrete pushes on the sheet; the frame holds it back. Got a column at an odd size, or a pipe that has to come through the wall? A carpenter cuts it on the bench in minutes. When the face wears out, you change the face and keep the frame.
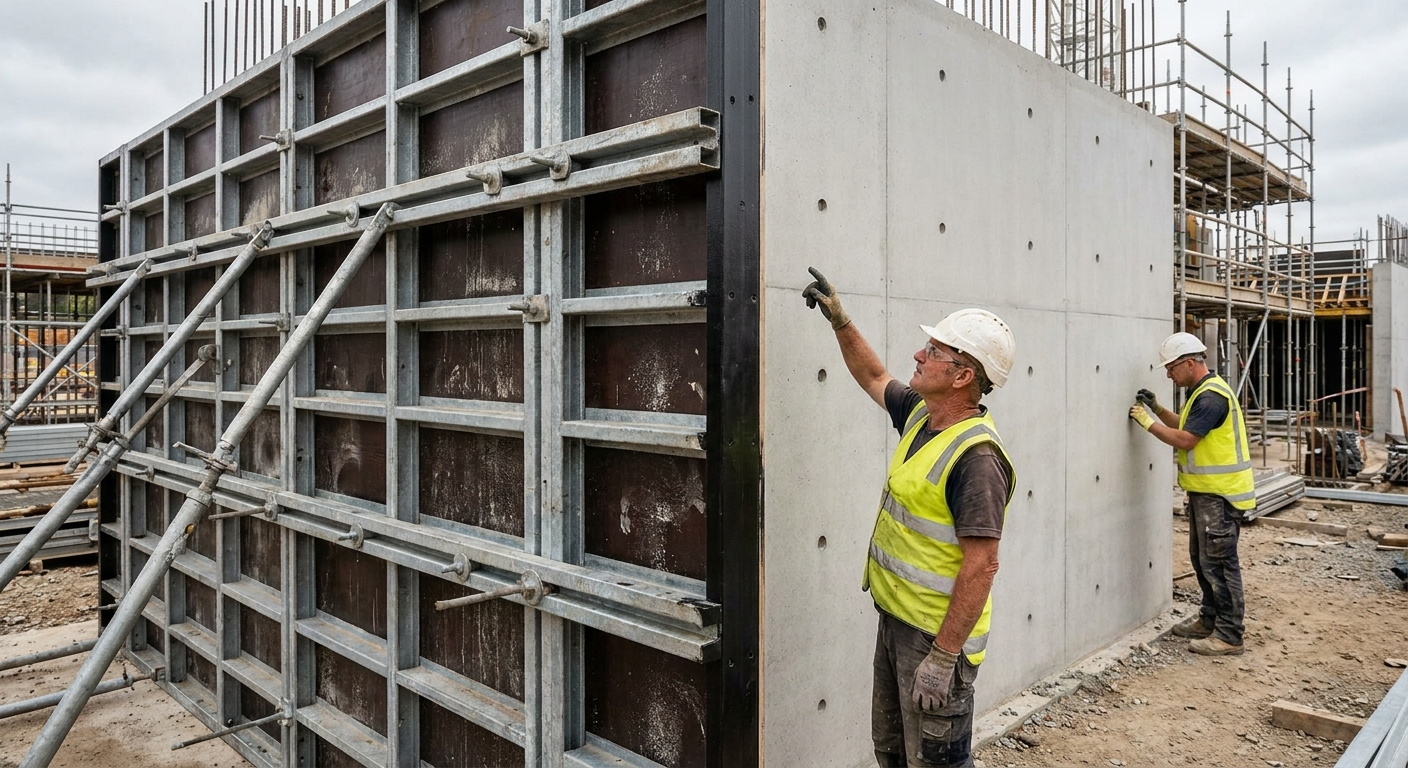
"Steel formwork" covers more ground than the name suggests. Sometimes the steel really is the casting skin. Often, though, and especially with the rented modular wall systems, it's a steel frame with a plywood or composite face fitted inside. Running that kind of kit? Then the real choice isn't steel or plywood. It's which face goes on the frame you've already got.
Cost per pour, not price per sheet
Forget the sheet price for a moment. What you want is cost per pour: the landed price of the form, plus edge sealing and face repair, divided by the pours it actually gives you, with handling labour on top. Cheap panels that die early can work out dearer per cast than better panels that go the distance. A steel set that never gets near its planned pour count? Often the priciest thing on site.
Plywood keeps the first cheque small. You buy panels by the container and start forming, no modular fleet to commit to. Steel means buying a system or signing a hire contract, and you pay for the steel and for the engineering behind it. Here's how the main options compare. Panel reuse numbers are maximums from our product data; steel and aluminium figures come from whoever makes the system, so take them from that vendor's data sheet.
| Option | Upfront cost | Reuse basis | What drives cost per pour | Weight and labour | Finish | Best fit |
|---|---|---|---|---|---|---|
| Film-faced plywood, MUF core (Eco Form Plus, Form Basic, Form Extra) | Price on request; lowest entry cost | Up to 8, up to 10 and up to 15 reuses; Class 2 bond | Edge sealing, stripping care, dry storage | Light; hand-set by two workers | Smooth phenolic film face | Footings, basements, short residential and retaining runs |
| Film-faced plywood, phenolic core (Pro Form Lite, Pro Form) | Price on request | Up to 15 (Pro Form Lite) and up to 20 (Pro Form); Class 3 bond | Same handling factors over a longer life | Light; suits faces on rented frames | Smooth phenolic film face | Repeat commercial walls, columns, hybrid frames |
| HDO plywood (HDO Basic, HDO Standard, HDO Premium) | Price on request | HDO Basic up to 10, Class 2; HDO Standard and HDO Premium up to 20, Class 3 | Face care and edge sealing | Light | Smooth, high-gloss off-form face | US forming work that needs a hard overlay |
| MatteFace Plywood (MTF) | Price on request | Up to 17 for MatteFace HD 1SF | Face care and edge sealing | Light | Even matte concrete face | US architectural walls with a matte finish |
| Steel modular panels | Capital purchase or hire | Vendor-rated; check the system data sheet | Pour count actually achieved, cleaning, coating upkeep | Heavy; crane-dependent for most sizes | Smooth while the face stays clean and coated | Very high repetition of one section |
| Aluminium modular panels | Capital purchase or hire | Vendor-rated; check the system data sheet | Pour count, face replacement | Lighter than steel | Depends on the face fitted | Repetitive housing and slab cycles |
Look hard at the steel row. Steel wins on cost per pour only if the job runs enough near-identical pours to soak up what it cost, and a lot of jobs don't come close. Think of a run of footings, or one retaining wall. A handful of casts, then the steel sits in the yard while a stack of film-faced panels would have finished and been gone. Our guide on how many times you can reuse formwork plywood walks through panel life grade by grade if you want the detail.
Why site habits decide how close a panel gets to its maximum
Treat the reuse numbers in that table as a ceiling, not a promise. Panels get close to them on sites where the crew handles forms like tools. They don't on sites where a form is something you rip off the wall and throw on the pile. A pry bar at the edge tears the film, water gets into the veneers behind it, and a few pours later the corner is soft. Unsealed cut edges swell after the first wet pour. Stack sheets flat on muddy ground and they soak up water from underneath before they've seen any concrete.
None of the fixes are expensive. Seal cut edges on the day you cut them. Oil the face thinly before each pour, strip with wedges or the system's own release hardware, and keep the stack off the ground and under a cover. We'd honestly rather a customer spent an hour a week on edge sealing than paid extra for a heavier panel to make up for rough handling, because the hour is cheaper and works better.
What sits under the face film
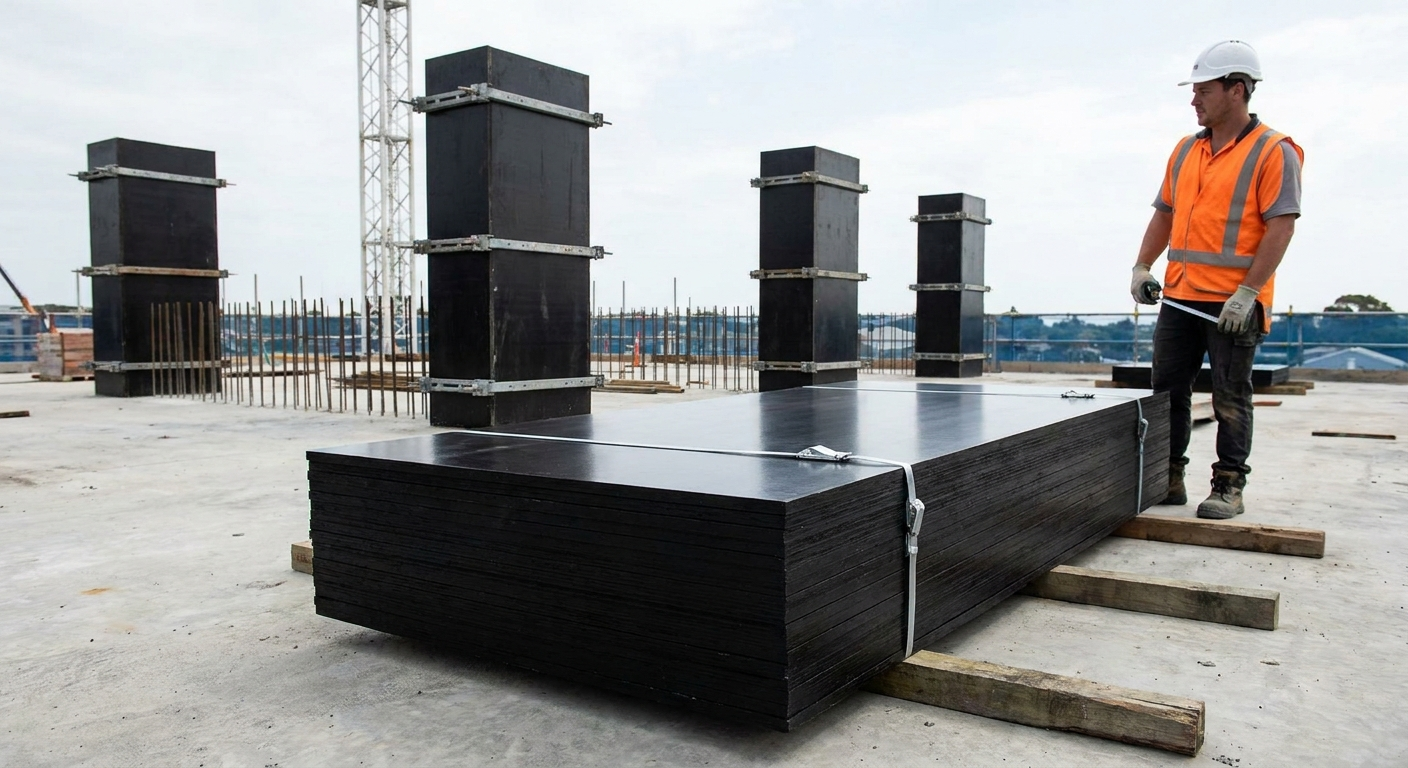
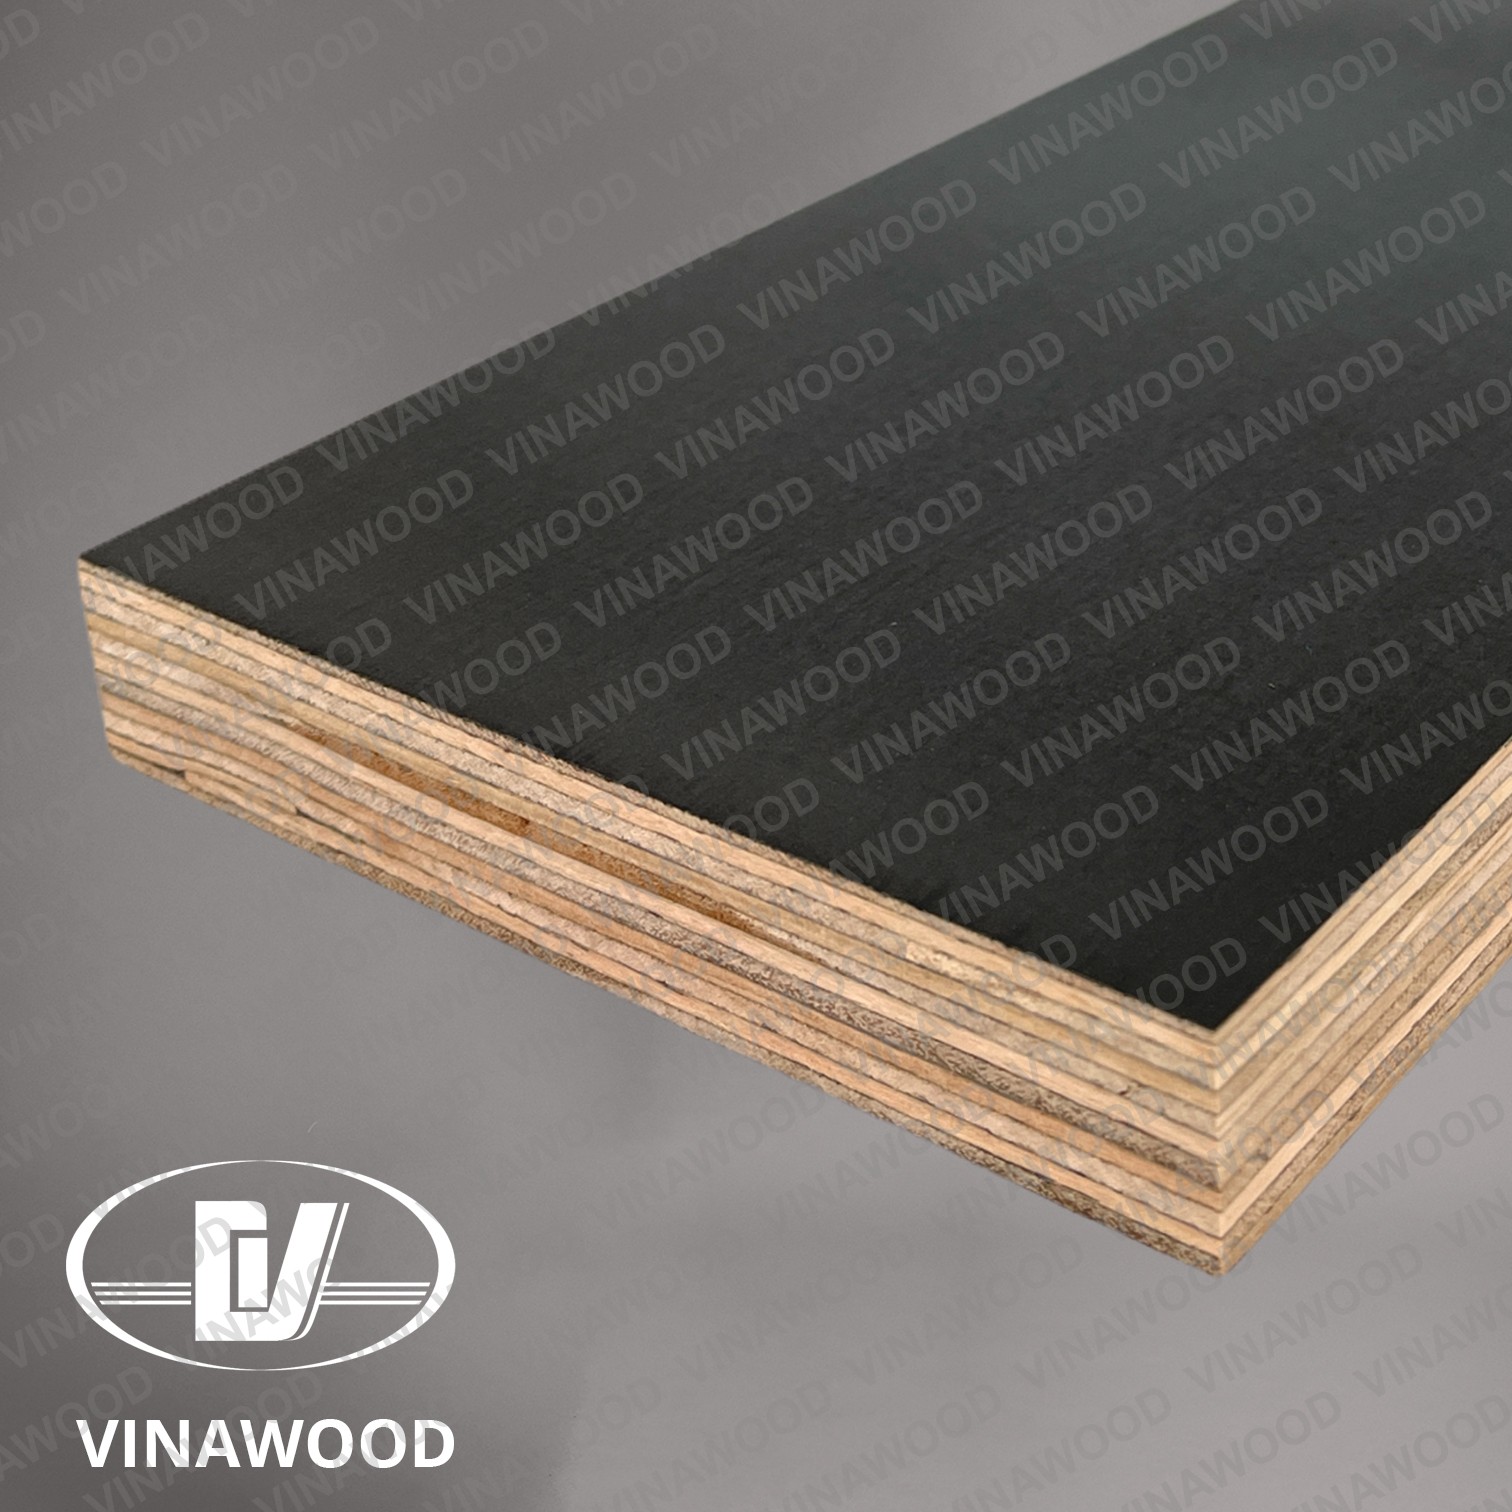
Every formwork panel we make has a phenolic face film, the dark smooth skin that meets the concrete. Where the grades part ways is underneath, in the glue between the core veneers. Eco Form Plus, Form Basic and Form Extra use an MUF core glue (melamine-urea-formaldehyde) and sit in bond Class 2 under EN 636-2. Form Extra outlasts Form Basic thanks to a stronger Superior Glue MUF core. Same face film, though, and still not Class 3.
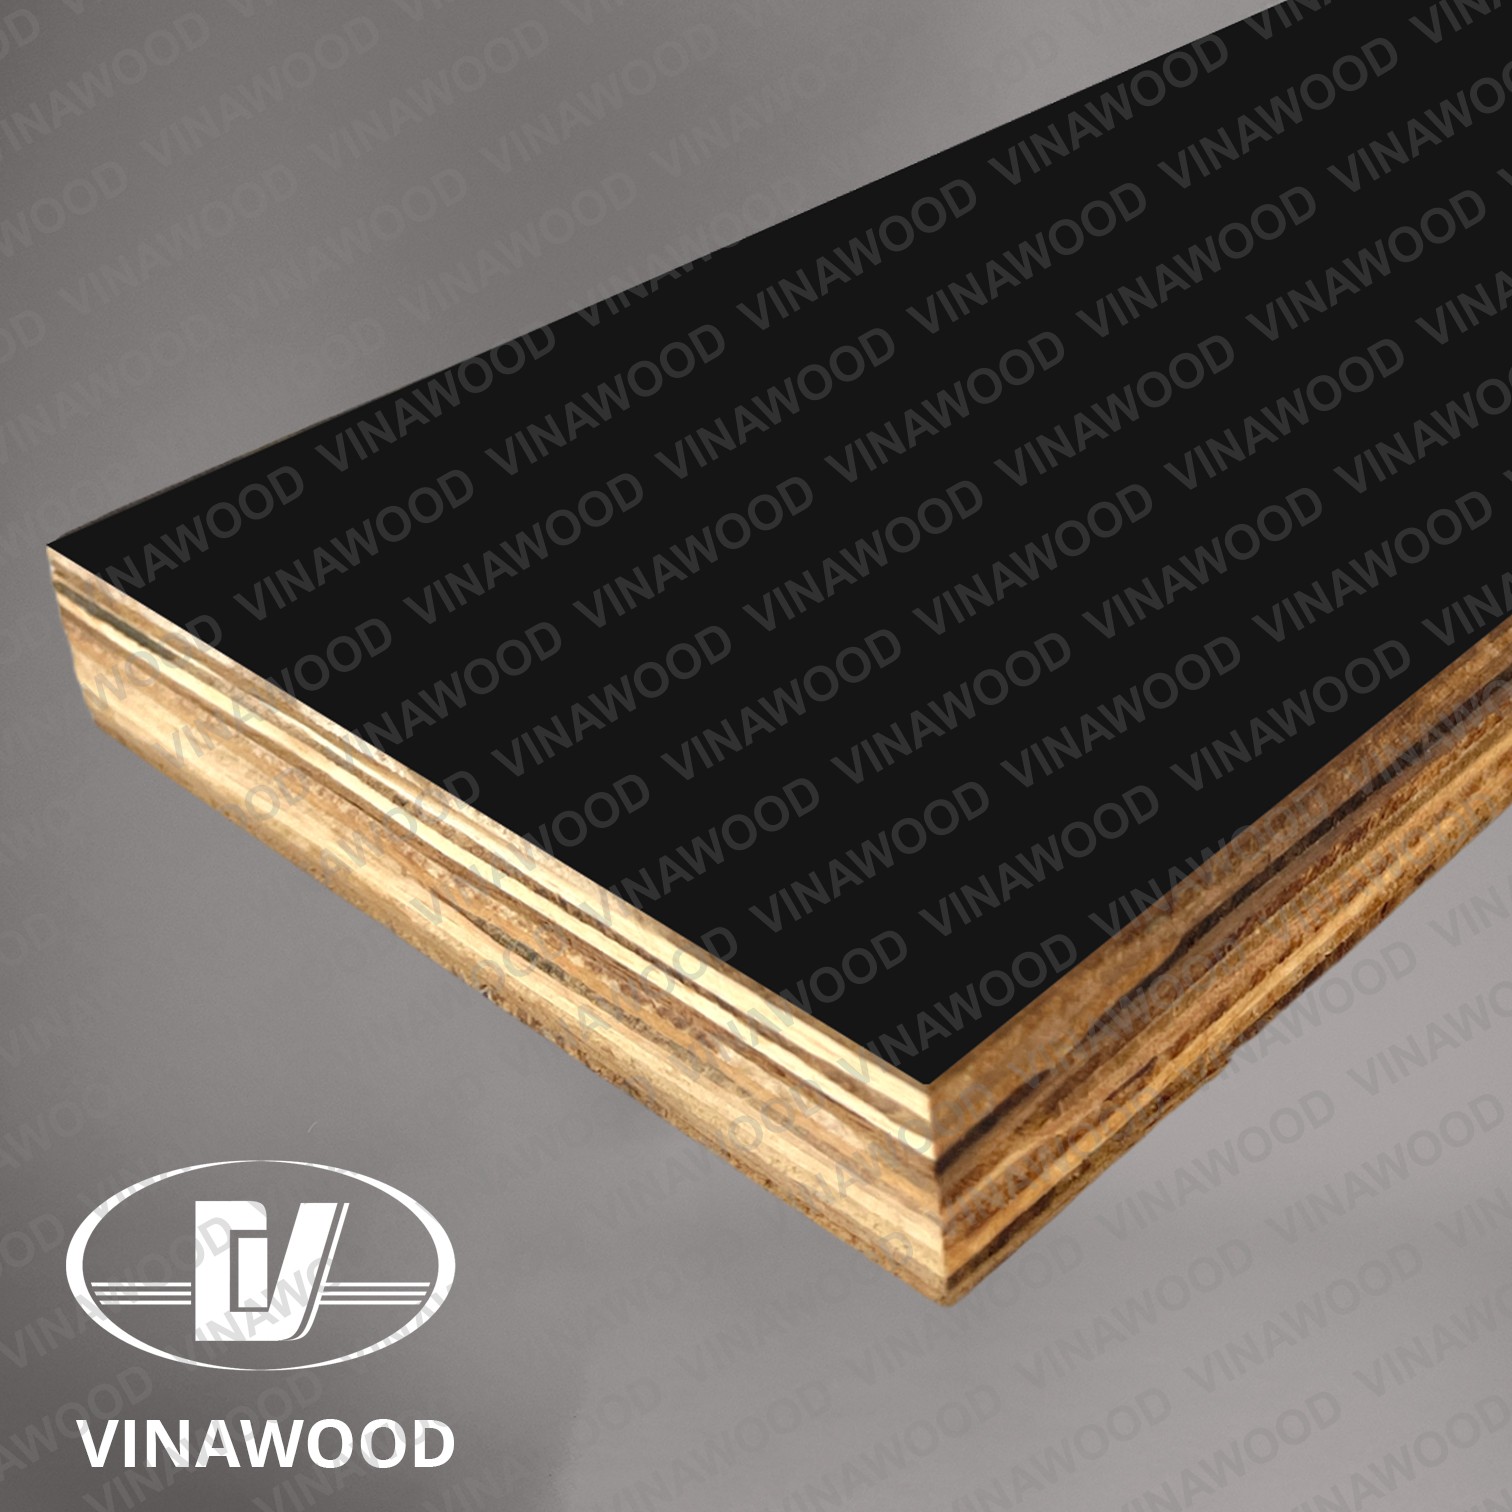
For Class 3 under EN 636-3 you need phenolic glue in the core, and in our range that means four panels: Pro Form, Pro Form Lite, HDO Standard and HDO Premium. HDO Basic trips people up. The family name is the same but the glue line is Class 2, so it isn't the answer to a Class 3 tender. Put face film and core glue on the RFQ as two separate lines; you'll avoid most of the arguments that start once the container lands. WBP glue gives you a water-resistant panel, and that's the property a form needs.
Concrete finish and what the face leaves behind
Keep a phenolic film face clean and lightly oiled and it casts smooth concrete for most of its working life. A steel skin manages the same, for as long as it's clean and the coating holds. When the coating fails it's a different story: rust can bleed into the wall, and a dent in the steel prints into every cast that follows.
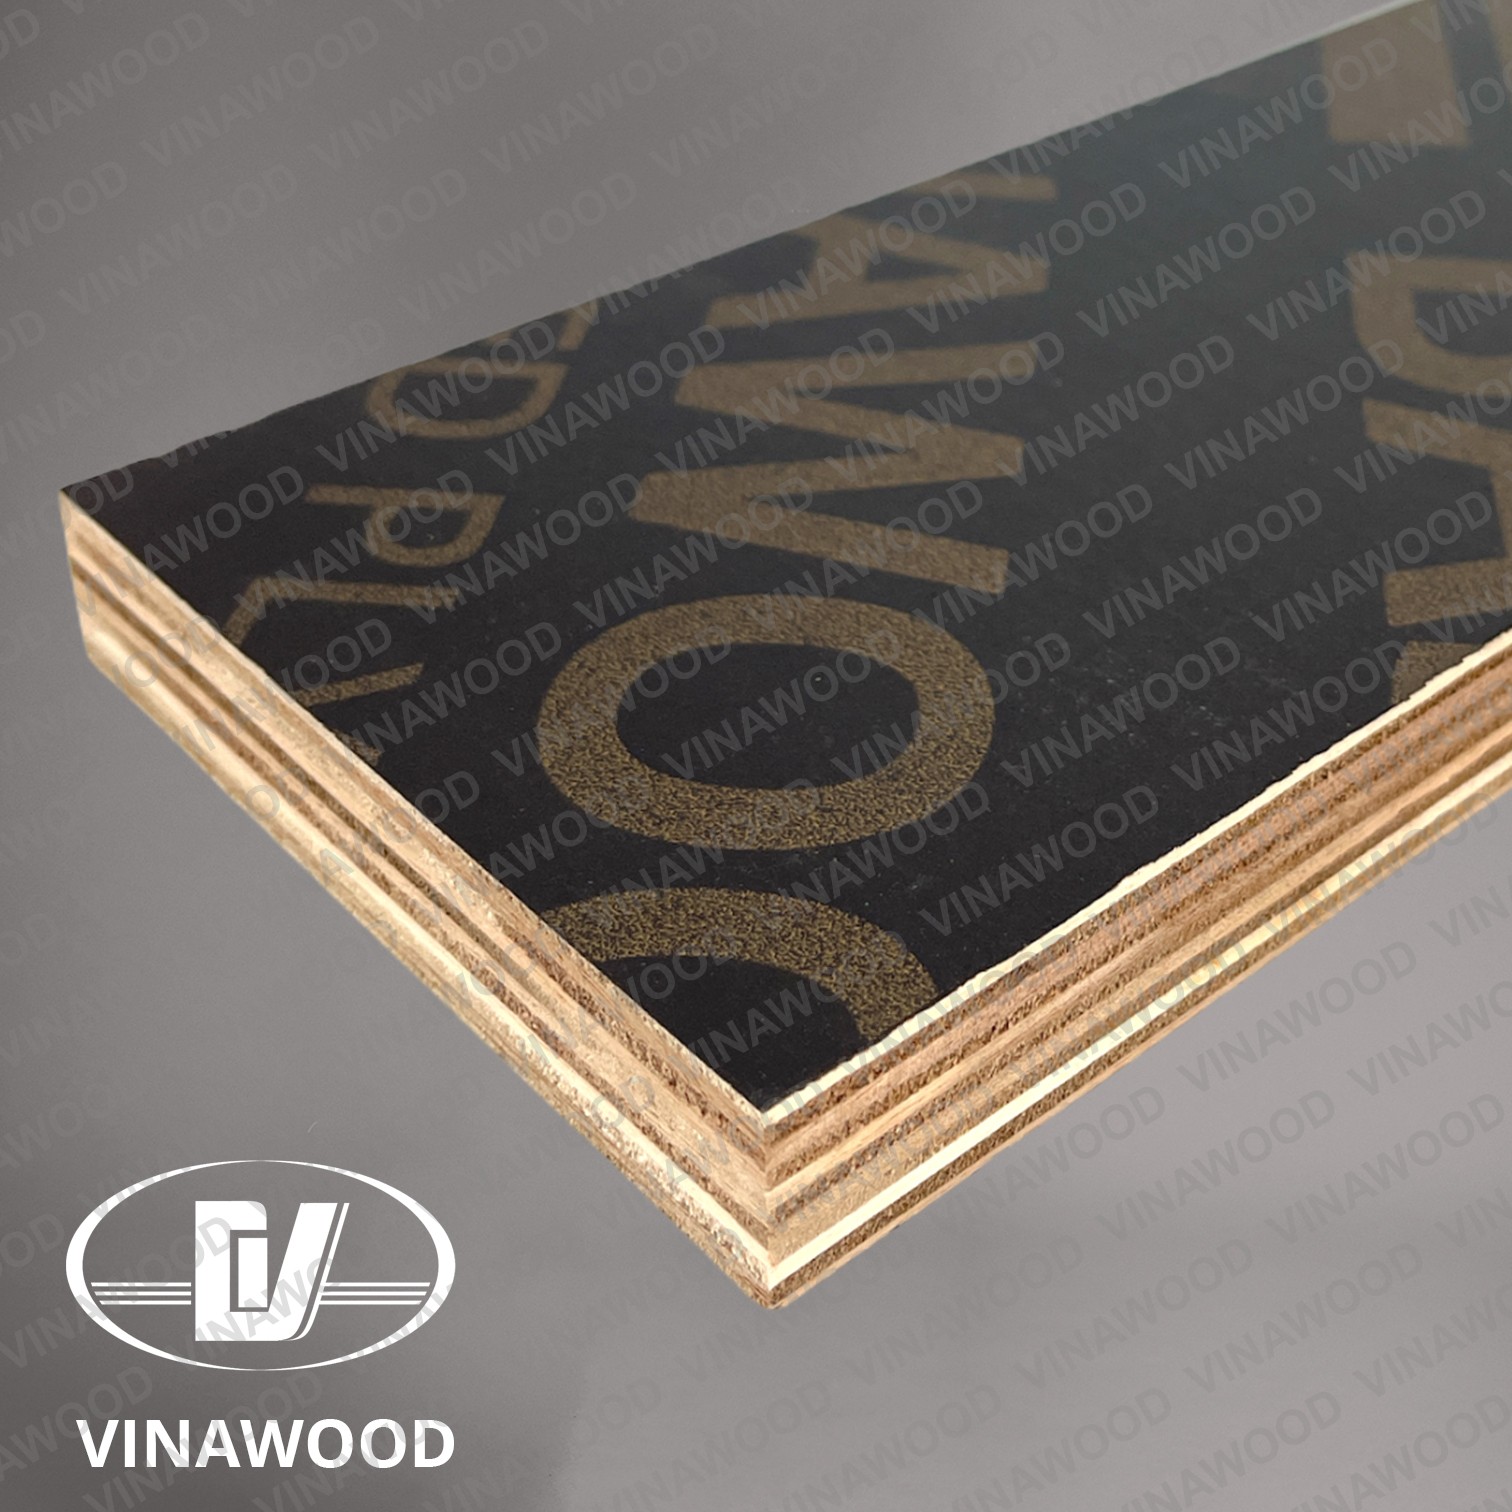
For exposed concrete, let the finish in the spec choose the face. Glossy off-form surface, go phenolic film-faced or HDO. A matte exposed wall is what MatteFace Plywood (MTF) is for, our matte phenolic surface film for formwork, which buyers often search for as MDO formwork plywood.
Weight and the pace of a pour cycle
A plywood panel is far lighter than a steel unit of the same size, light enough that two people carry an 18 mm sheet flat between them. Strip-and-reset goes quicker and the crane gets called less. On a tight site with a small gang, that tends to matter more than the theoretical pour count of the form.
Steel's weight is deliberate. It's built to last long programmes, and mass is what buys that. The catch comes when the crane is busy somewhere else and every cycle has to wait. Put the same gang form on a dedicated crane, same lift every week, and the weight hardly registers.
Choose plywood or steel
Write the pour programme down and the answer usually falls out of it.
Plywood-faced forms make sense when:
- each form sees a moderate number of pours, not hundreds;
- the geometry changes from level to level (blockouts, odd columns, curves);
- panels go up by hand and crane time is scarce;
- you already rent steel or aluminium frames and just need new faces;
- the spec calls for smooth or matte off-form concrete.
Steel makes sense when:
- one section repeats at very high volume, like a precast yard or a tunnel lining;
- handling is so rough a panel face would never reach its rated life;
- tight tolerances repeat often enough to justify steel's stiffness.
Aluminium falls in between. It's lighter than steel, popular for repetitive housing and slab cycles, and it usually carries a replaceable face, which puts you right back to choosing a panel.
Specifying the plywood option for a US job
Repeat-pour commercial walls, or faces going onto a rented frame, call for a Class 3 panel. In the US range that's HDO Standard or HDO Premium from the HDO plywood collection, or Pro Form Lite and Pro Form from the film-faced plywood range, plus MatteFace Plywood where the wall needs a matte face. A few pours of residential or retaining work? Form Basic or Form Extra will usually do it at a lower cost per pour.
We keep distribution warehouses in Toronto, Vancouver, Calgary, Montreal, Miami, Houston and Baltimore, and they hold ready stock for local distributors, so a container programme can be topped up locally when a job runs short. Production runs under ISO 9001. Panels carry CE marking under EN 13986 for European work and meet CARB P2 and TSCA Title VI for the US. Send us the pour programme, the finish class and the frame system, and we'll suggest a panel and prepare a quotation.
Category
how-to
Related Markets
Related Countries
Related Products
▶Sources & References (2)
- ACI PRC-347-14(21) Guide to Formwork for Concrete — American Concrete Institute (2021)
- EN 636:2012+A1:2015 Plywood. Specifications — European Committee for Standardization (CEN) (2015)