Concrete Forming Plywood: HDO, MDO & Film Types
Concrete forming plywood explained for buyers: which wood does which job in a concrete form, the phenolic, film-faced, HDO and MDO (MatteFace) type ladder, and how to spec overlay, bond class, size and emission class. Vinawood, Vietnam, since 1992, 55+ countries.
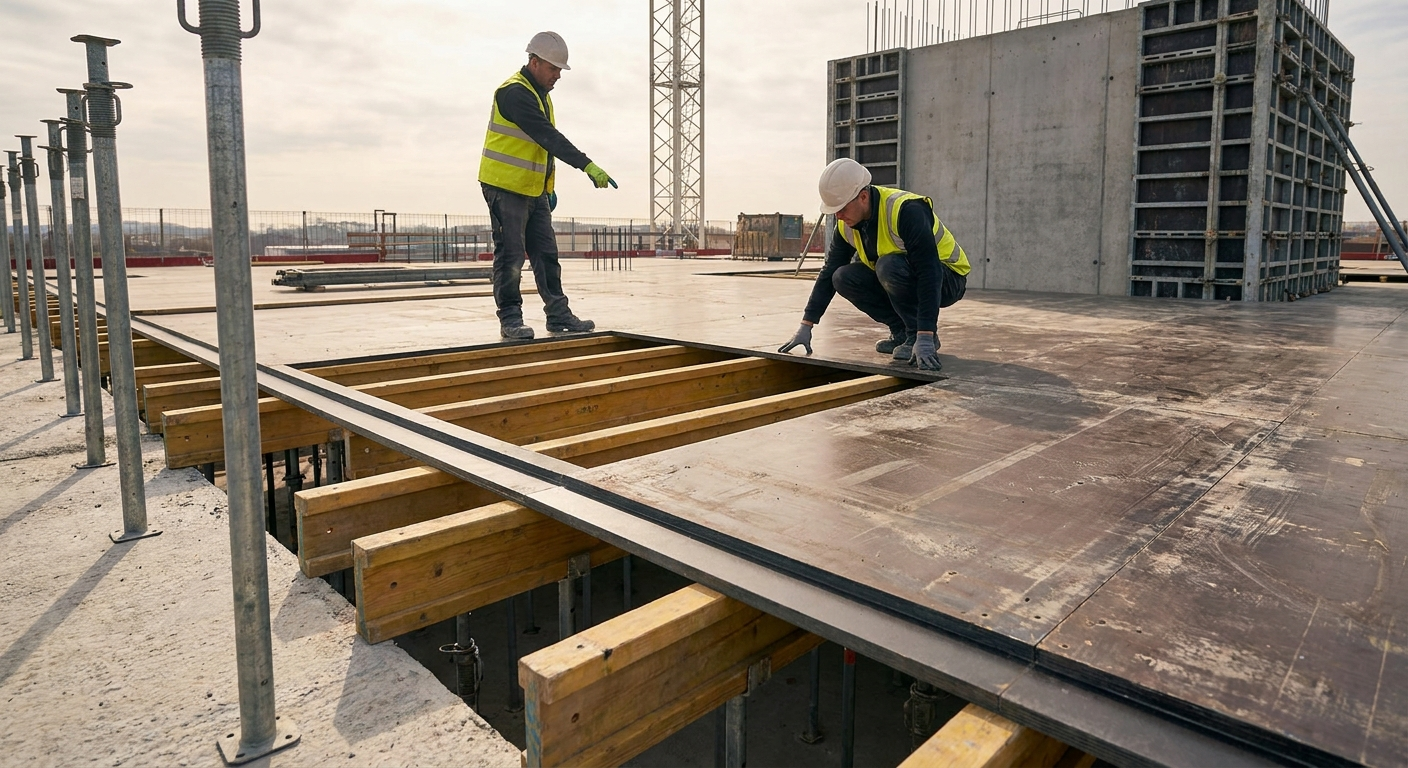
Concrete forming plywood is the overlaid sheet a crew pours against: the temporary mold face that holds wet concrete until the pour can carry itself. It soaks up the pressure of fresh mix, leaves its own texture on the finished wall, and then has to strip clean so the gang can move up a lift. Whether a panel lasts on your job is decided before anyone talks price. Four things settle it: the overlay on the face, the glue class in the core, the sheet size your frames expect, and the emission class your paperwork needs.
Names change by market, the sheet doesn't. A US take-off says forming plywood or plyform; UK and Indian sites say shuttering; export price lists say film-faced. Below we sort those names into one ladder (phenolic film, HDO, and the matte face people still search for as MDO) and match each rung to the Vinawood grade that ships against it. Contractors sizing a specific wall may prefer concrete form plywood, UK readers the shuttering plywood guide, and researchers the atlas overview of Vietnam formwork plywood.
What wood is used for concrete formwork?
Two kinds of wood do two separate jobs in a concrete form: sawn lumber or engineered timber beams carry the load, and plywood is the face the concrete touches. On walls, that means studs plus walers, the horizontal members tying a gang together. On slabs it's timber joists like H20 beams resting on steel props. Only the plywood ever meets the mix. So its face and its stiffness are what you end up looking at once the forms come off.
Old bridge piers still show board grain, because boards were the first form faces. They lost out for a simple reason. A solid board cups when one side is wet and the other dry, and then it splits along the grain. Plywood is built from thin veneers with each layer's grain turned 90 degrees to the next, and that cross-lamination keeps an 18 mm (3/4 in) sheet flat between joists under a full pour. Our forming cores are plantation-grown Acacia or Eucalyptus (Hevea on some lots), chosen for exactly that balance.
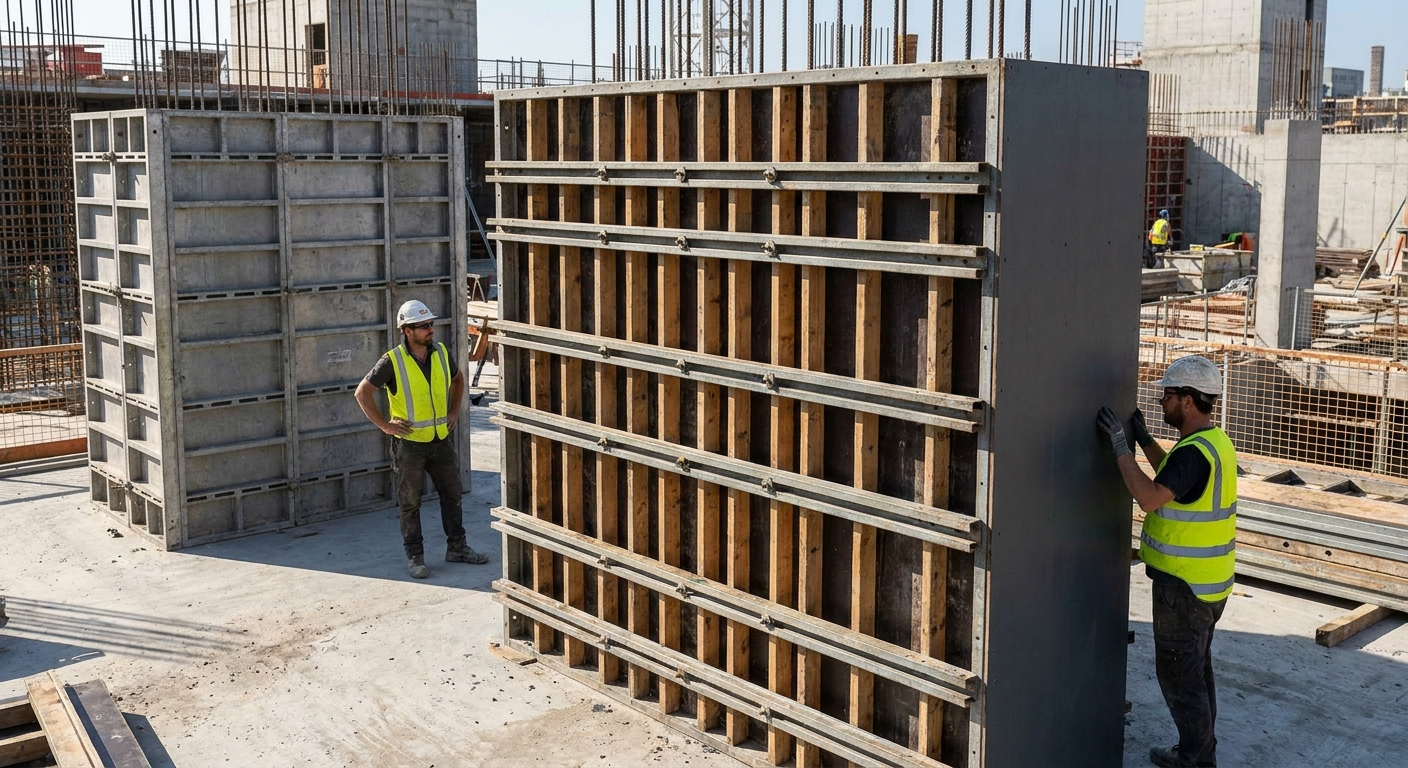
Big wall gangs from system suppliers now run steel or aluminum frames. The face, in most cases, is still plywood. It can be cut, drilled, patched or swapped on site when a corner gets knocked, which a welded face can't. Vinawood panels go onto framed systems from Doka, Peri and Alsina wherever the sheet module matches the frame, and the cases where all-steel or plastic faces win are laid out on formwork plywood alternatives.
How a forming panel is put together
Think of a panel type as four fields rather than "three layers glued into a board," a shortcut that still turns up on trader quotes and hides everything important. The core is the veneer stack. The overlay is the resin face that sets the finish and keeps water off the wood. Then there's bond class (how the glue line behaves when soaked) and emission class (what the customs file and the green-building auditor want to see).
Bond class is where most RFQ mix-ups begin, because it has nothing to do with what the face looks like. EN 636-2, or Class 2, panels carry MUF (melamine-urea-formaldehyde) resin in the core. EN 636-3, or Class 3, panels carry phenolic PF resin. Put a phenolic film over an MUF core and you still have Class 2; that is precisely what Form Extra is. On our list, Class 3 means Pro Form, Pro Form Lite, HDO Standard and HDO Premium, nothing else, and when a Class 2 sheet lands on a wall specified as Class 3 the glue line tends to be what fails first.
"Melamine" on a forming quote is a trap of its own. It might mean MUF in the core. It might mean a melamine-impregnated face film, or the printed decorative laminate on a kitchen door. Ask which. Form Extra uses a higher-melamine MUF core we call Superior Glue under a phenolic face, so it's a weather-rated formwork panel, just not a Class 3 one.
Formwork plywood type ladder: phenolic, film-faced, HDO and MDO
Buyers tend to compare prices across trade names before checking what sits behind each one, and that's how a sanded sheet ends up quoted against an overlaid panel. The table maps every common name to the grade that answers it. Reuse numbers are mill maxima, so we write them as "up to N"; rough handling and skipped release agent will eat that life well before the overlay wears through.
| Trade name | What buyers usually mean | Vinawood grade | Reuse (maximum) | Bond class |
|---|---|---|---|---|
| Plyform / budget forming | Low-cost face for a short pour series | Eco Form Plus or Form Basic. Sanded BB/OES plyform is not a Vinawood SKU | Eco Form Plus up to 8; Form Basic up to 10 | MUF, EN 636-2. Not Class 3 |
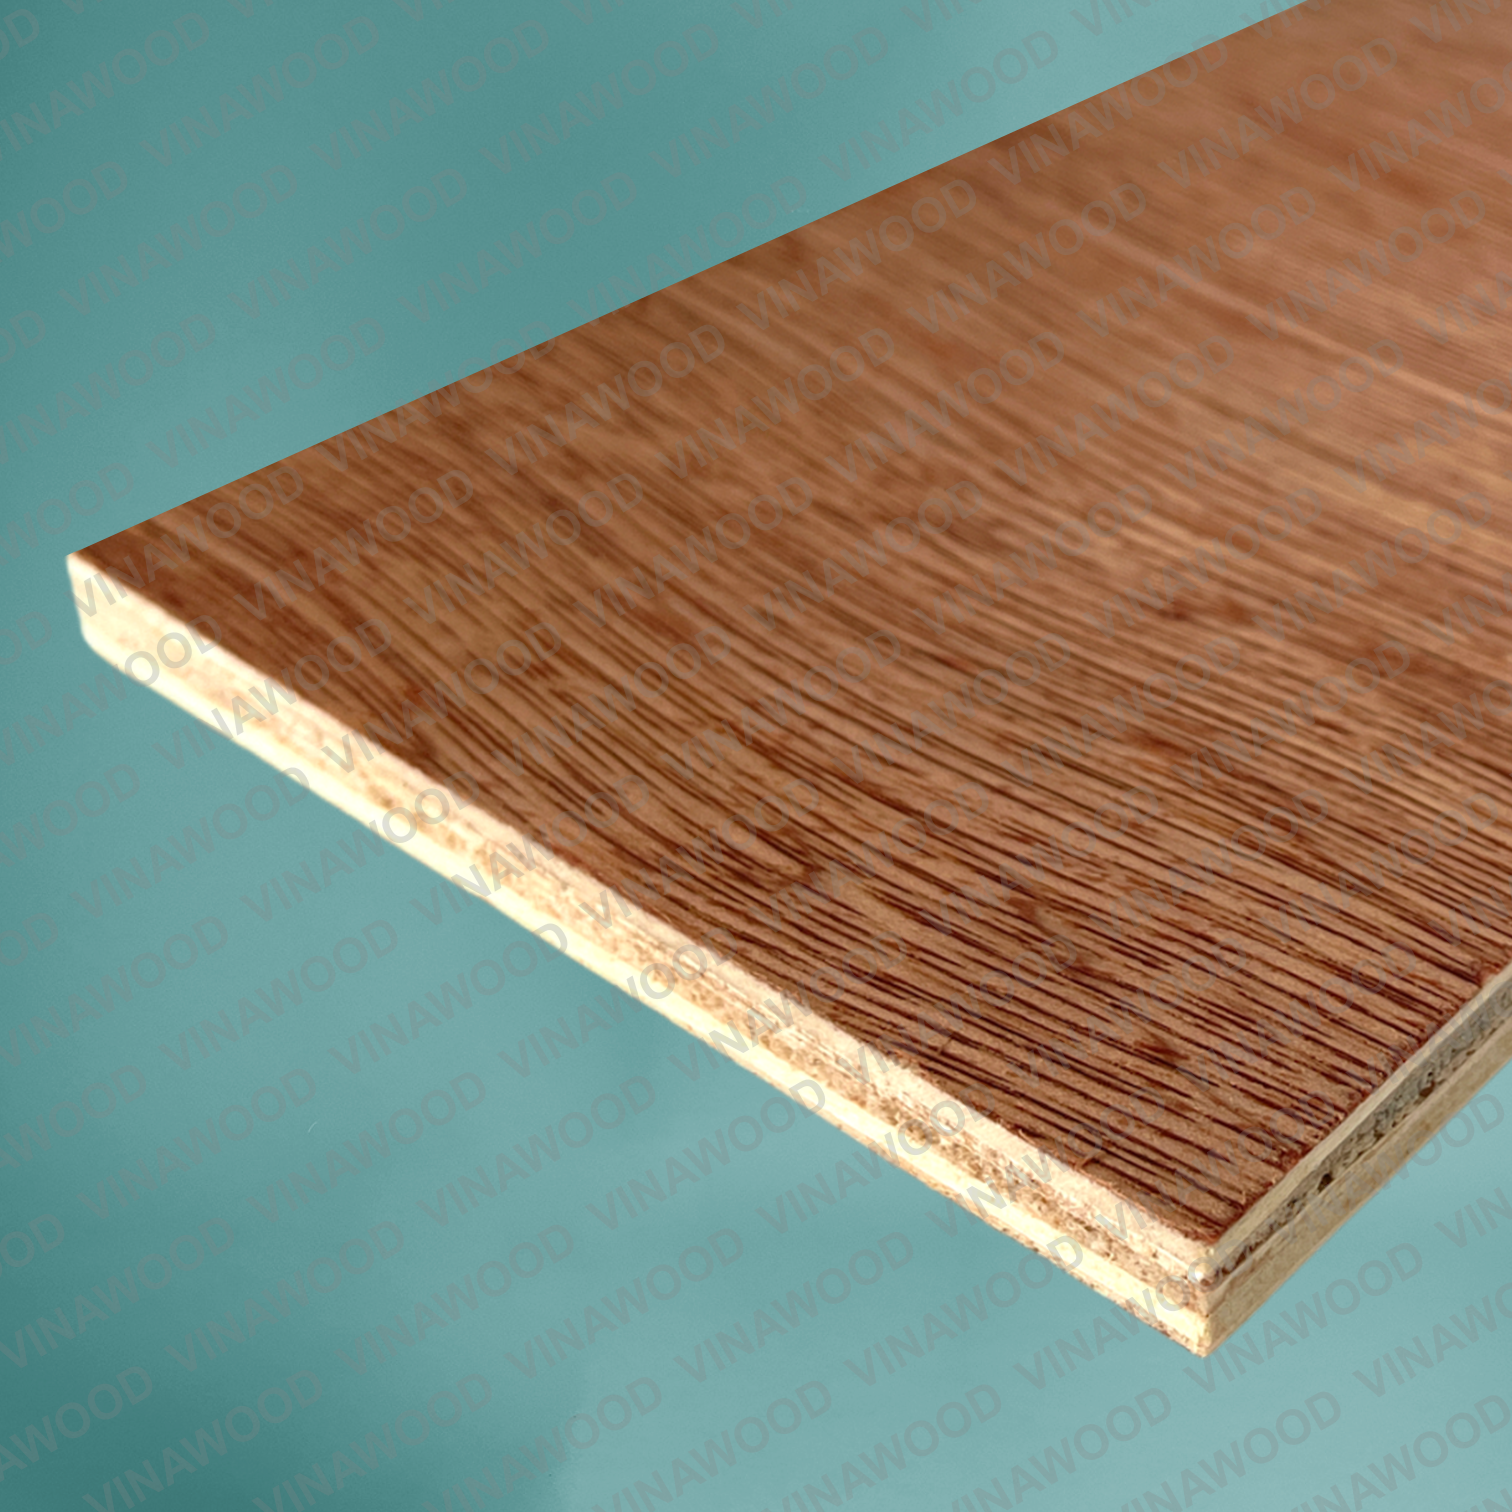
| MDO (search term) | A matte form face, not kraft-paper sign board | MatteFace Plywood (MTF). Buyers often search for MatteFace as MDO formwork plywood | up to 15 | Matte phenolic surface film; formwork only |
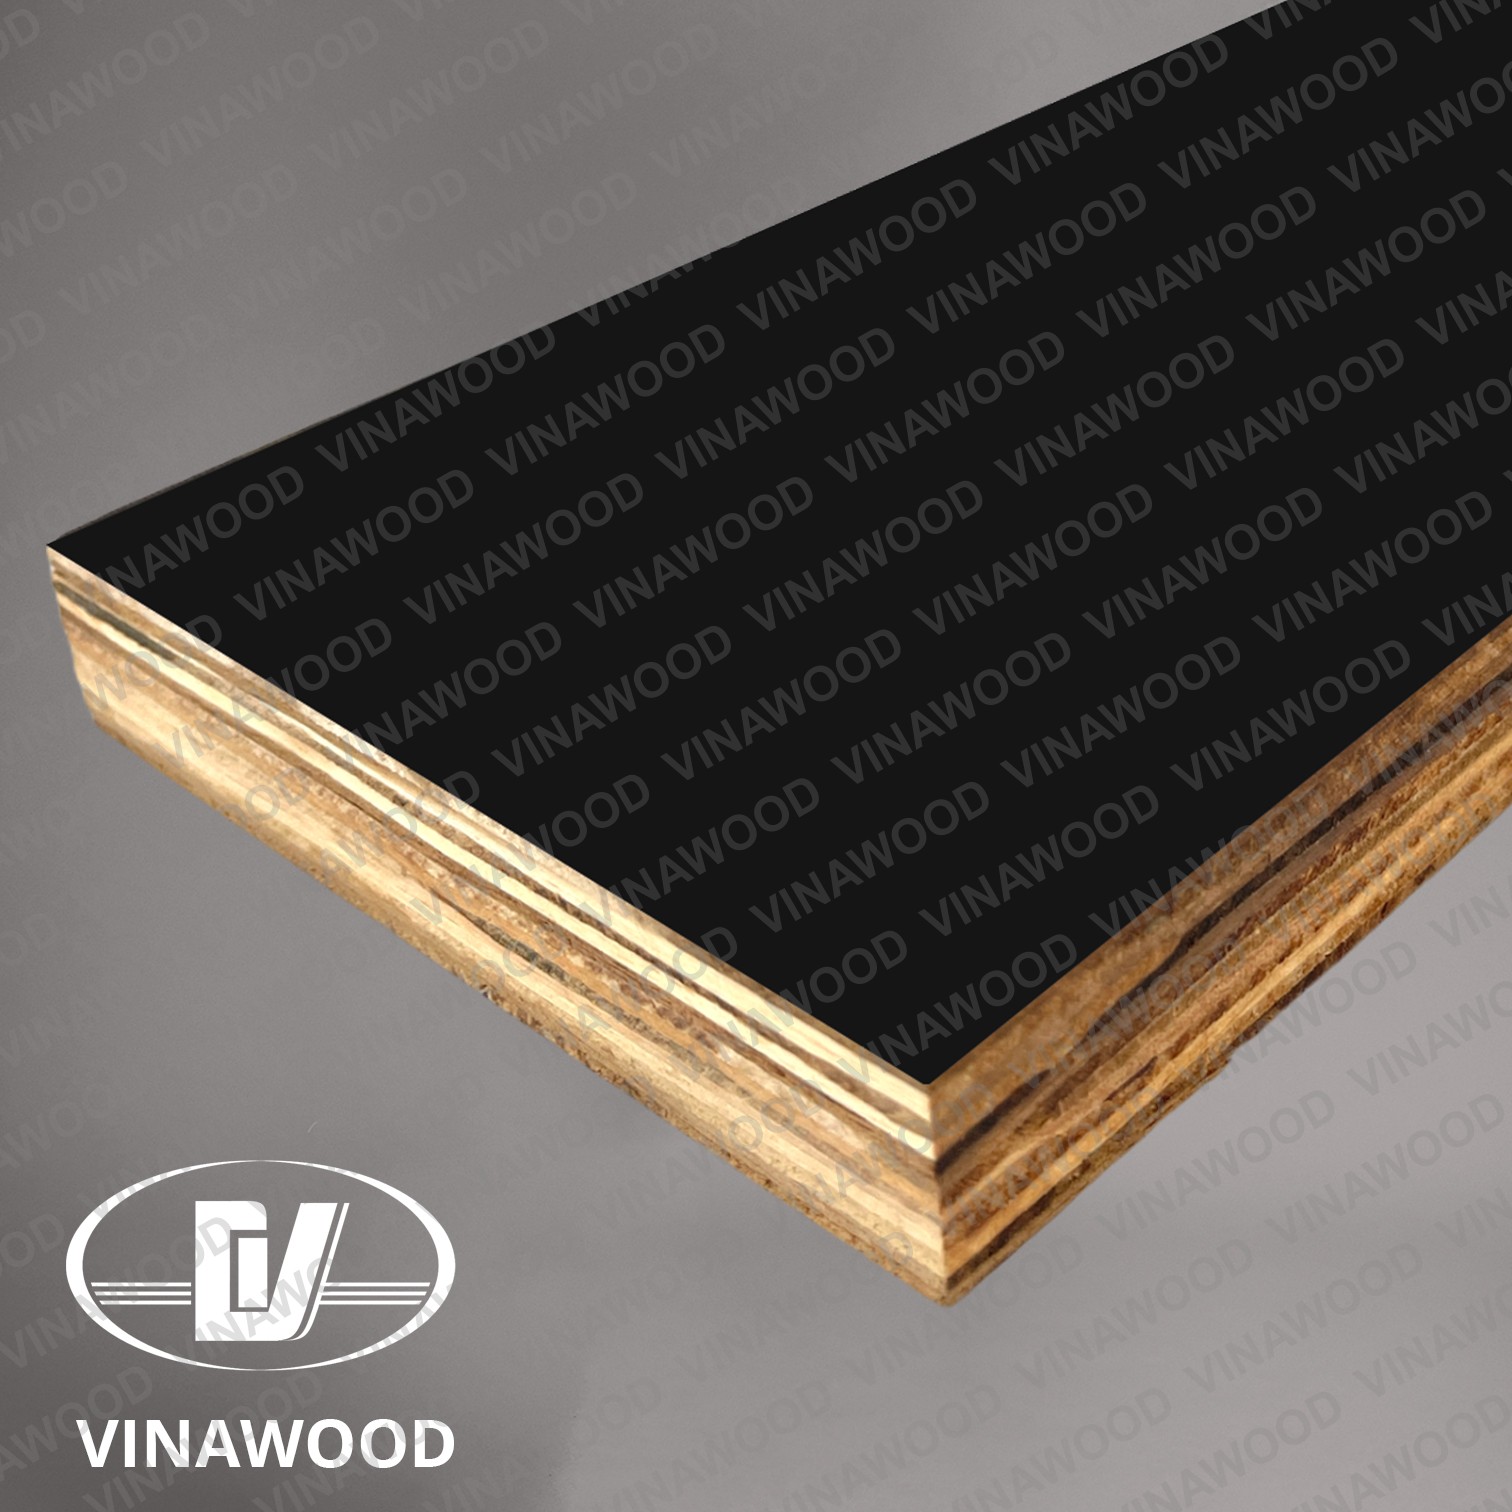
| HDO | High-density overlay for glossy fair-face concrete | HDO Basic, Premium, Premium HD | Basic up to 10; Premium and Premium HD up to 20 | Basic: Class 2 (EN 636-2); Premium and Premium HD: phenolic PF, Class 3 (EN 636-3) |
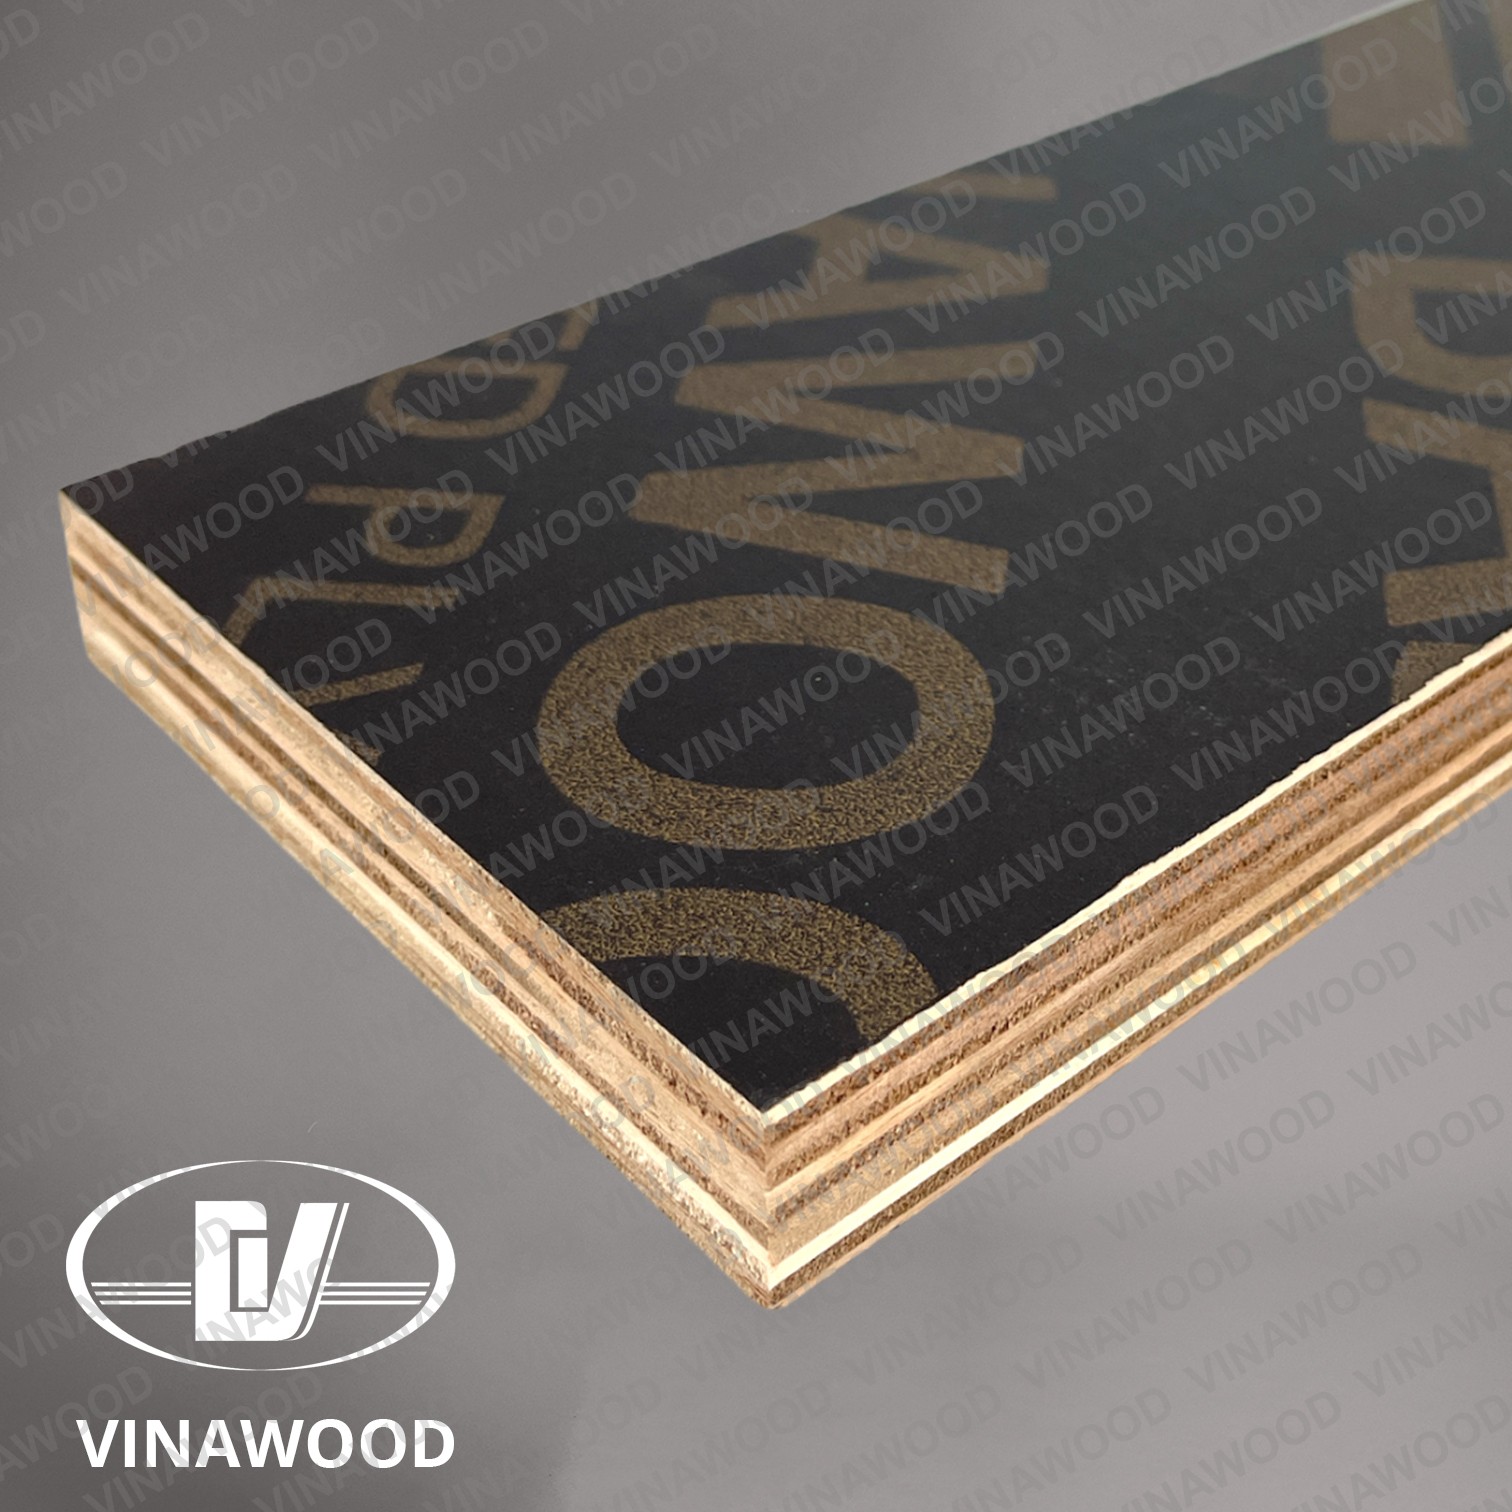
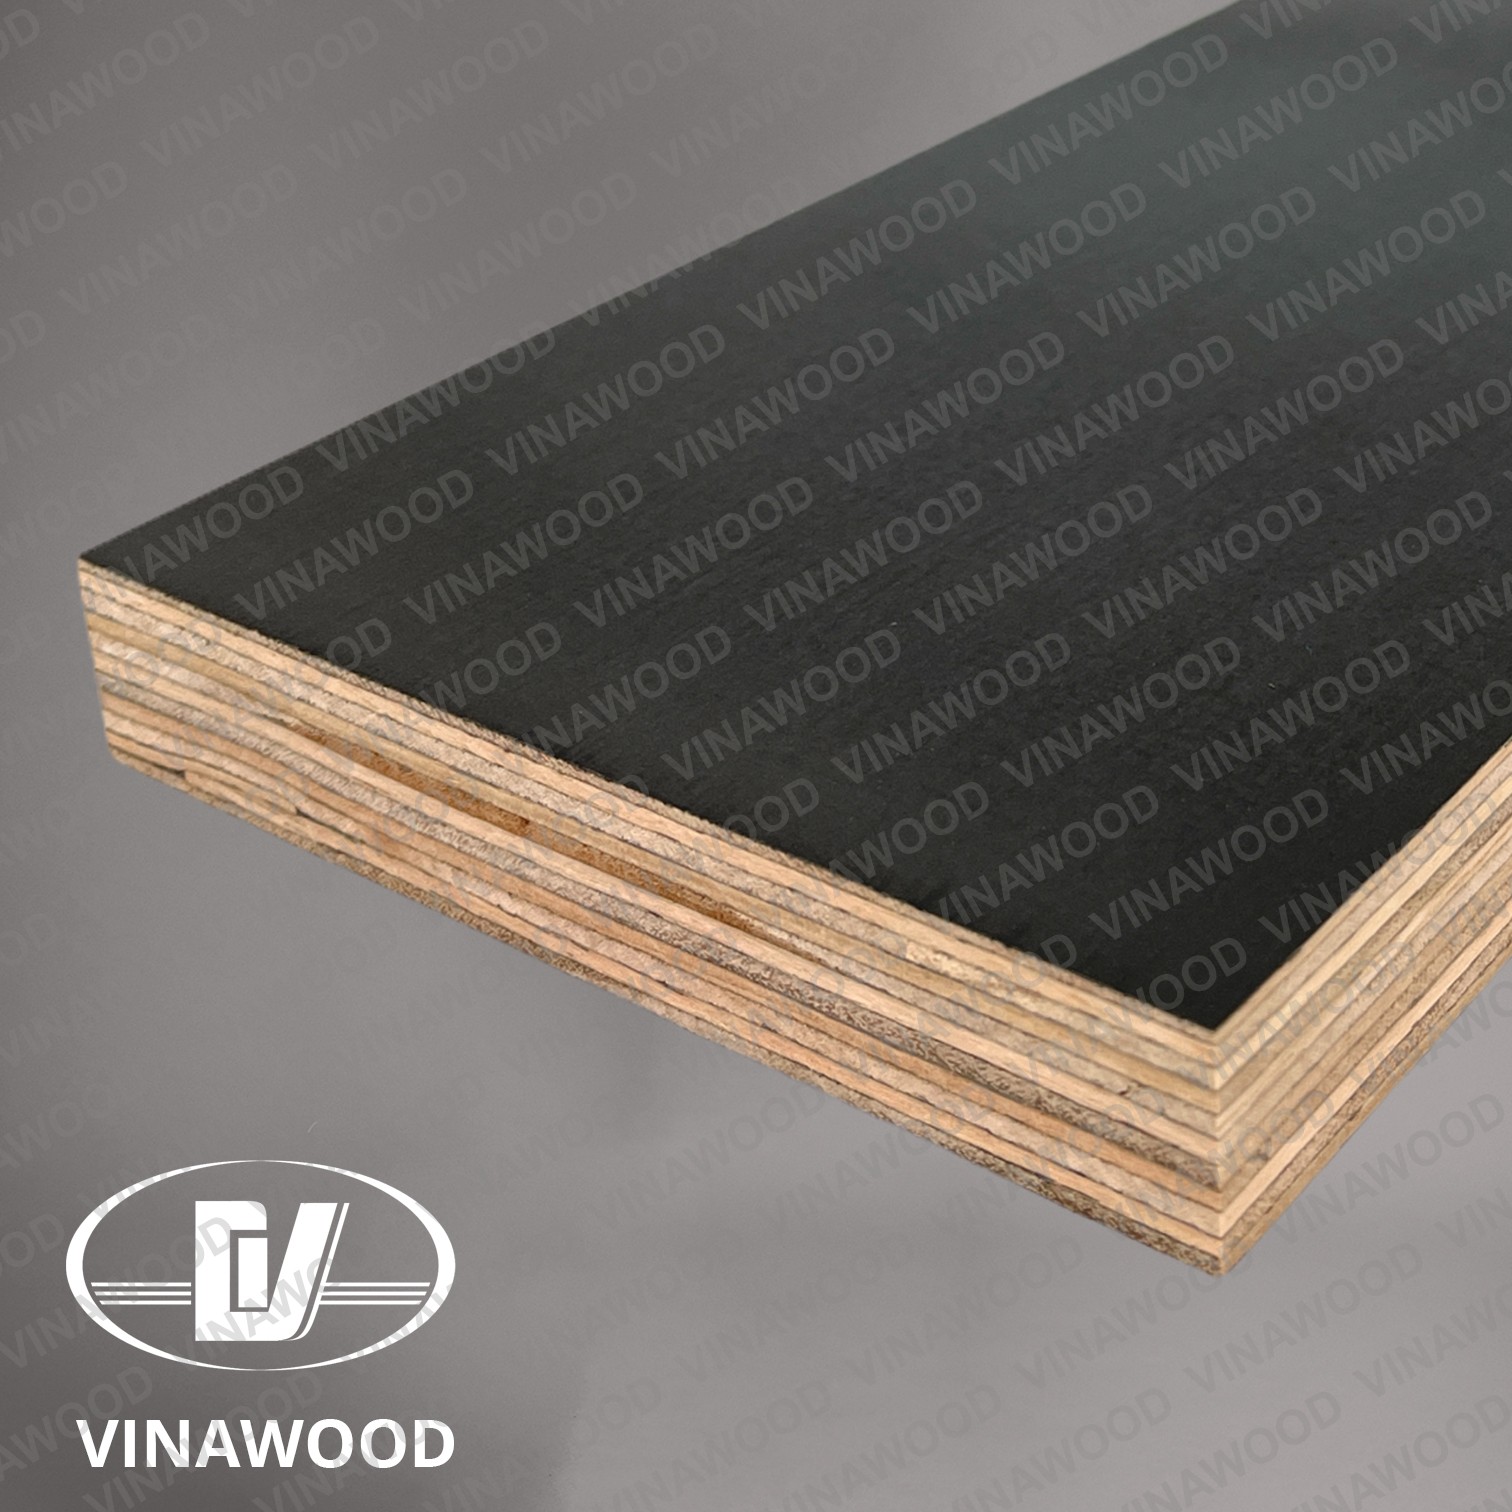
| Film-faced / phenolic face | Resin film face for reusable wall and slab forms | Form Extra, Pro Form Lite, Pro Form | Form Extra and Pro Form Lite up to 15; Pro Form up to 20 | Form Extra: Superior Glue MUF, EN 636-2. Pro Form Lite and Pro Form: PF, Class 3 |
No single brand word picks the right type. A buried footing nobody will ever see is fine on Eco Form Plus or Form Basic. Matte architectural walls point to MatteFace; glossy North American fair-face points to HDO. High-rise cores that cycle the same gang for months usually land on Form Extra or one of the PF grades, depending on how wet the site runs. In every case it's cost per pour that decides, not the invoice for the first container.
How concrete plywood forms are specified on a job
A spec for concrete plywood forms travels a long way, from estimator to trader to mill and back, and loose wording like "good quality formply" usually returns as the lowest-priced sheet anyone could find. Write the overlay first, since it fixes both finish and reuse ceiling. Next, name the bond class as EN 636-2 or EN 636-3 so nobody can slip a weaker glue line behind an identical face. Then the size: module, thickness, tolerance, all matched to the frames already sitting on site.
Emission class is the field people forget until a shipment is held. US lots need CARB P2 / TSCA Title VI. CE-marked lots need EN 13986 on the Declaration of Performance, and projects that track chain of custody will want FSC-COC or PEFC on the order too. These don't replace overlay or bond class. They sit on the same line.
Written down, those four fields also give the site manager something to check a delivery against, so a wrong lot gets rejected at the gate instead of discovered on the third pour. It's also why our sales team asks for the pour programme with every enquiry. The planned cycle count tells us which rung is the honest recommendation, and sometimes it's a lower-priced one than the buyer expected.
Advantages of concrete forming plywood
Stiffness for its weight is the headline. Cross-laminated veneer handles panel shear far better than solid timber at the same thickness, yet an 18 mm sheet at 1220 × 2440 mm (4 × 8 ft) is light enough for two people to place by hand, which counts on a busy deck when the crane is booked for rebar. Calibration sanding before the overlay keeps thickness steady from sheet to sheet, so a long wall doesn't show a step at every joint.
Reuse comes next, though only when it's tied to an overlay. Our maxima climb from up to 8 pours (Eco Form Plus) and up to 10 (Form Basic, HDO Basic) to up to 15 for Form Extra, Pro Form Lite and MatteFace, then up to 20 for Pro Form and HDO Premium. Those are ceilings. A bargain sheet that dies at pour four turns out to be the dearest panel on the job, and the film economics behind that are worked through in advantages of film faced plywood.
Finish and weather behaviour round it out. The form face becomes the concrete face, so grain, patches and scratches all print; fair-face drawings need HDO, MatteFace or a PF film written on the RFQ before price comes up. WBP, short for weather and boil proof, describes how the glue survives a boil test. It makes a panel water-resistant, not sealed against water, so seal every cut edge and keep stacks covered in humid yards.
What plywood is used for forming?
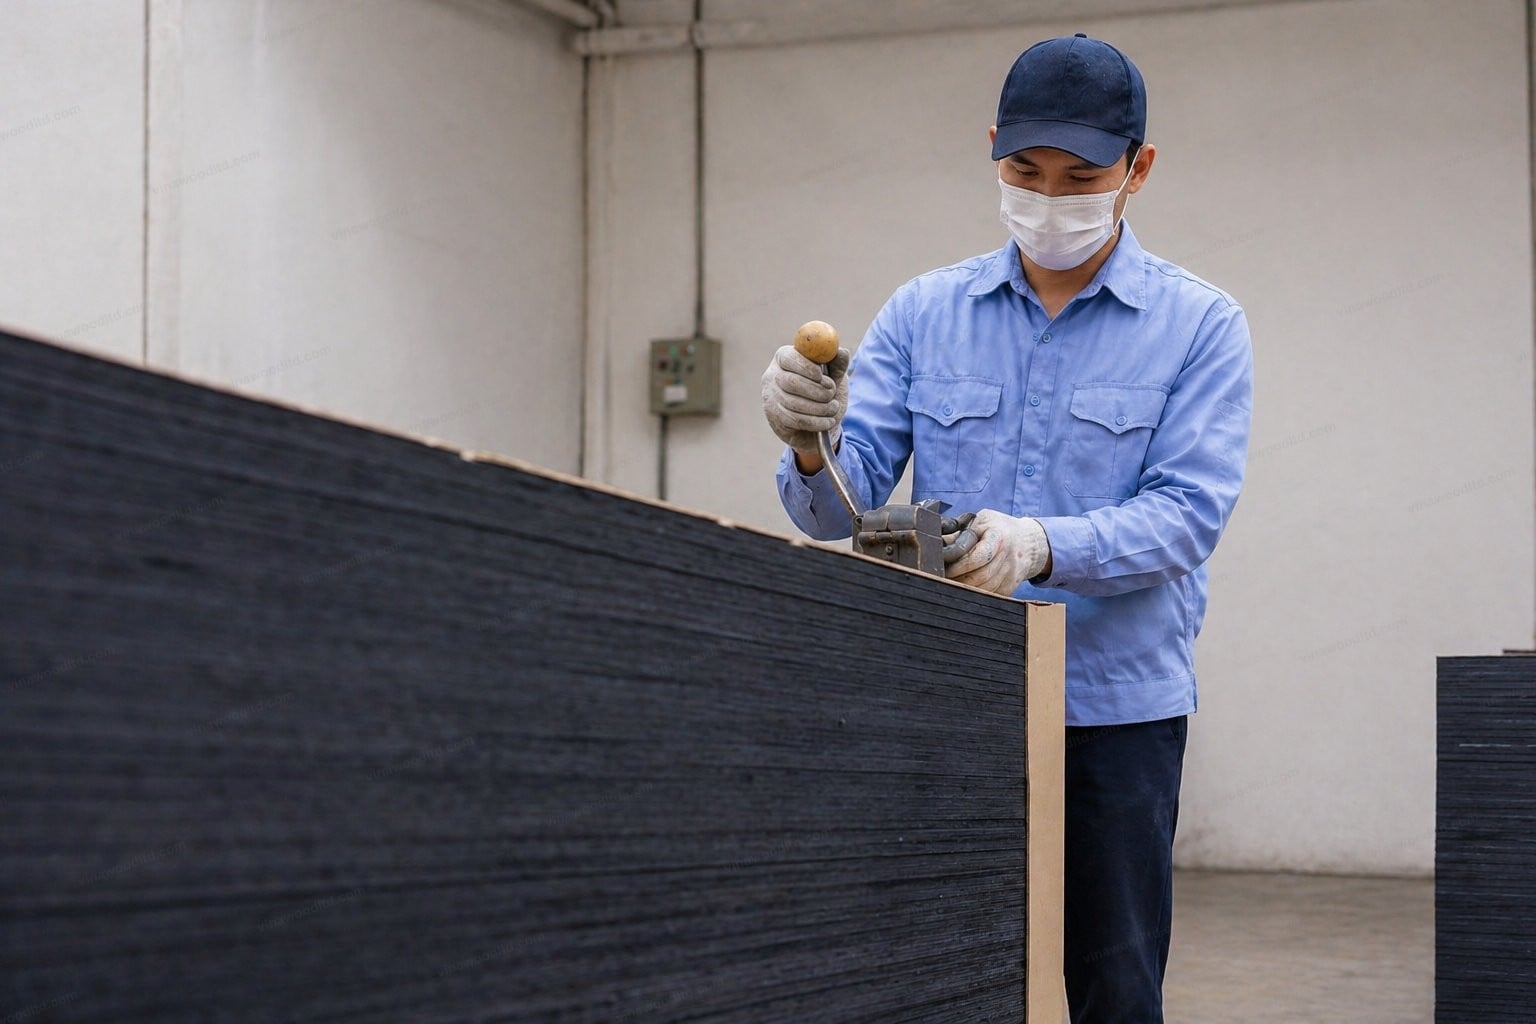
Most take-offs land on one of four overlay families, and steel, aluminum or plastic are separate system choices rather than grades of plywood. Inside plywood the real question is how much work you want the face to do and how many times the programme needs each sheet back.
HDO (High-Density Overlay)
HDO plywood is what North American crews reach for when the concrete will be seen. The resin-dense face is harder than a kraft overlay, takes knocks better, and strips glossy. Our HDO Basic is rated up to 10 reuses on a Class 2 bond, and HDO Premium and Premium HD up to 20 on a phenolic Class 3 core. Grades live on the HDO plywood collection; the matte comparison is on HDO vs MDO plywood.
MDO (Medium-Density Overlay)
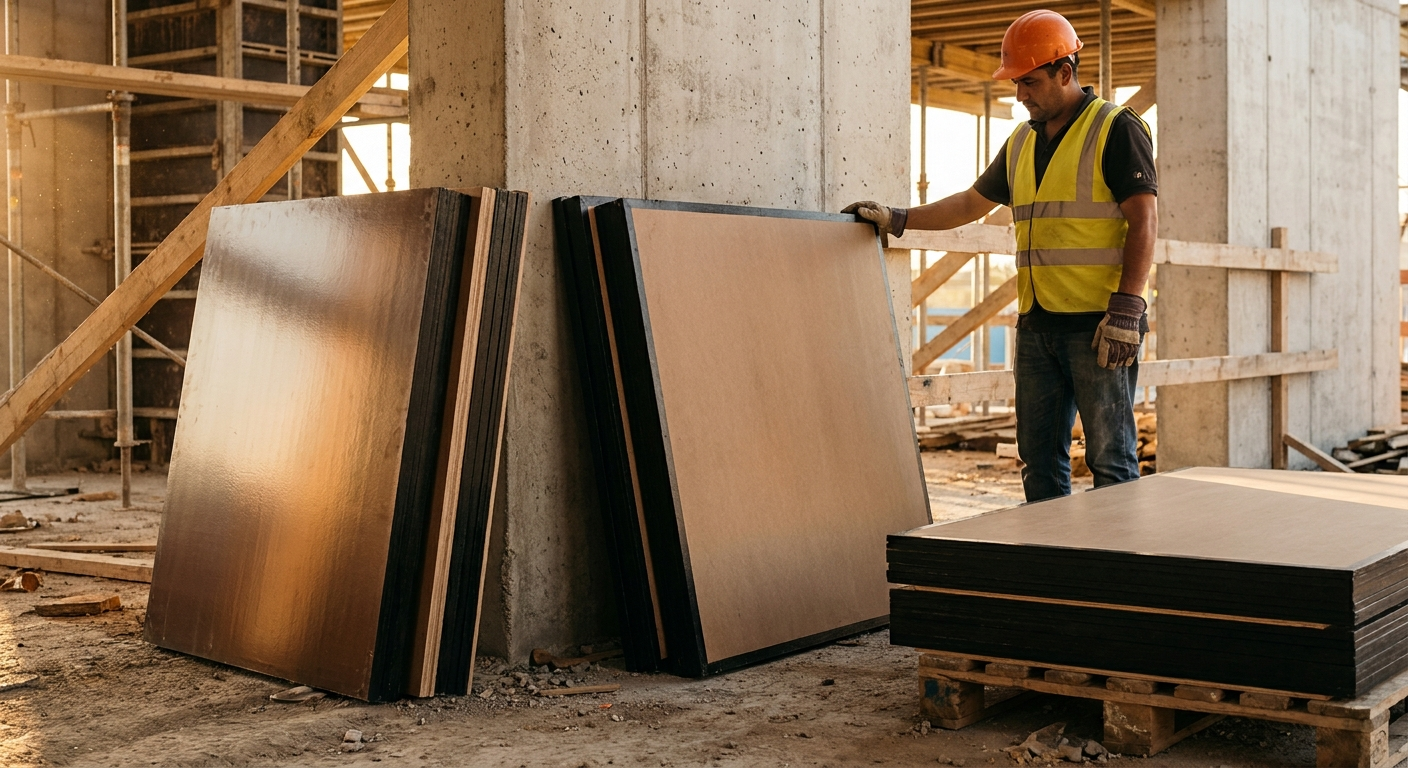
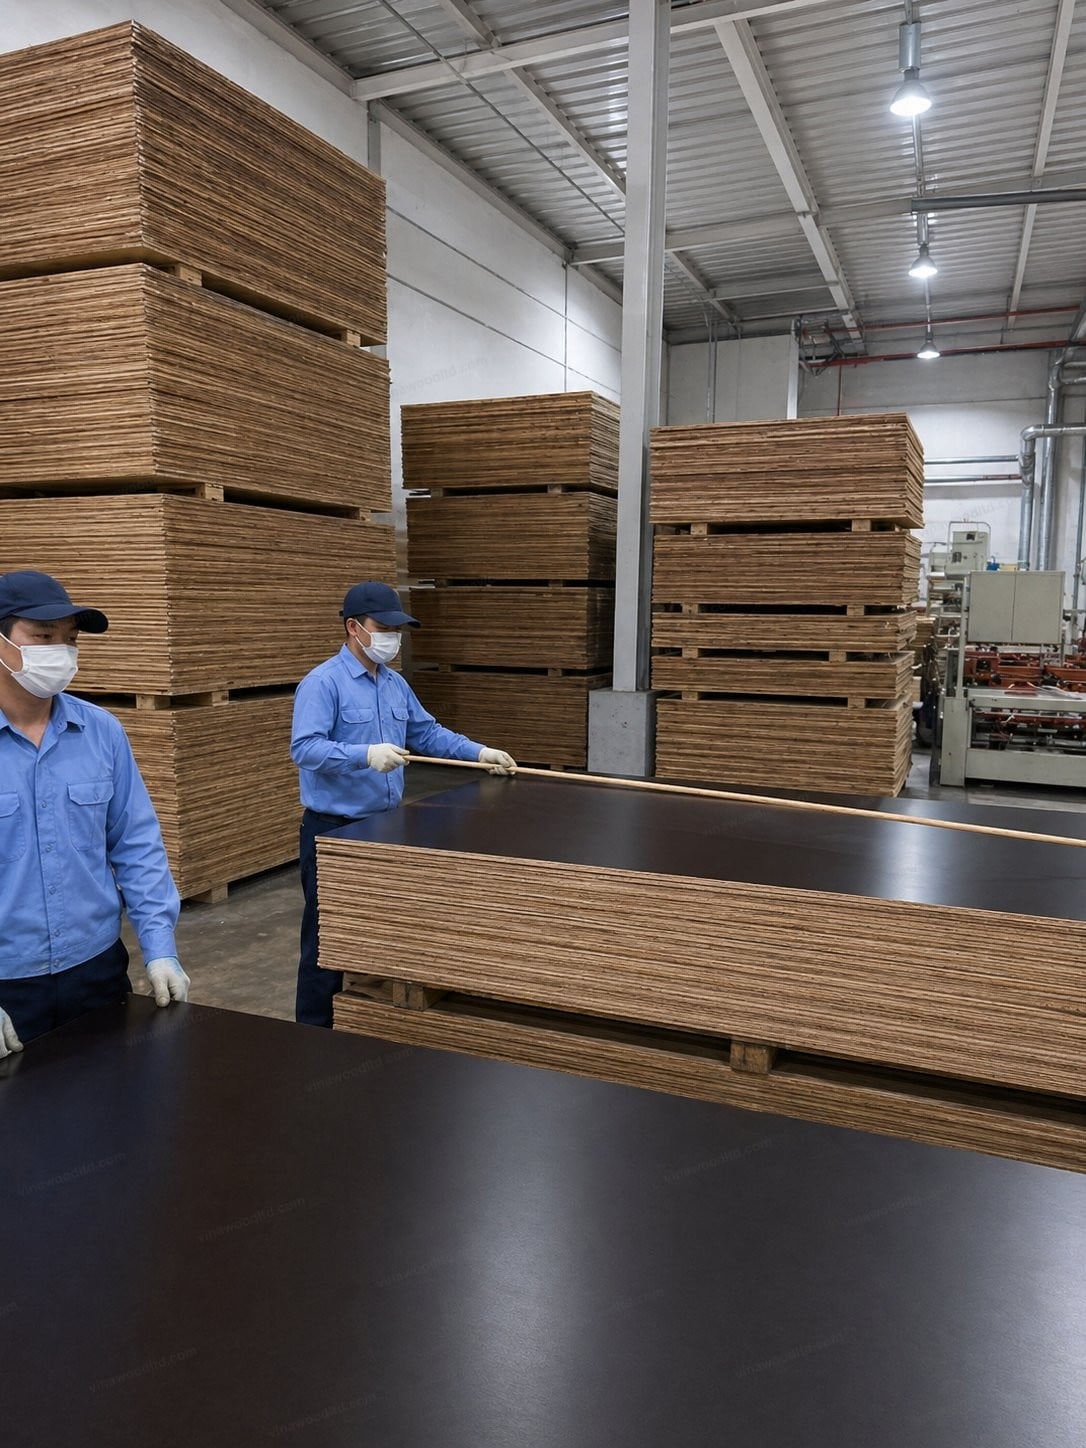
MDO covers two unrelated products, which explains a lot of confused quotes. Kraft-paper MDO is a paintable overlay for signs and siding. A forming crew wants something else: MatteFace Plywood (MTF), a matte phenolic surface film rated up to 15 reuses, not kraft paper and not for paint. Buyers often search for MatteFace as MDO formwork plywood. The overlay itself is explained on MDO plywood.
We still see RFQs with "MDO" on the product line from buyers who mean a matte phenolic form face. We quote those as MatteFace and confirm the finish before booking, because kraft-paper MDO comes from a different mill category altogether.
Film-faced and phenolic
Read the film and the core separately; a phenolic face film does not make a panel Class 3 by itself. Pro Form pairs WBP phenolic glue with EN 636-3 performance and up to 20 reuses. Pro Form Lite slots between Form Extra and Pro Form as a PF, Class 3 panel rated up to 15. Form Extra also reaches up to 15, but on Superior Glue MUF to EN 636-2. Form Basic shares Form Extra's phenolic face over a regular MUF core and is rated up to 10, and the value grade, Eco Form Plus, up to 8. See the film-faced plywood collection and, for site setup, the film faced plywood concrete formwork guide.
Two names trip people up. P-Form is polypropylene-faced and unrelated to Pro Form. Consply is a commercial Bintangor-faced board, not a film-faced formwork grade. A quote that calls either one Class 3 phenolic formply should go back for correction.
BB/OES plyform and marine plywood
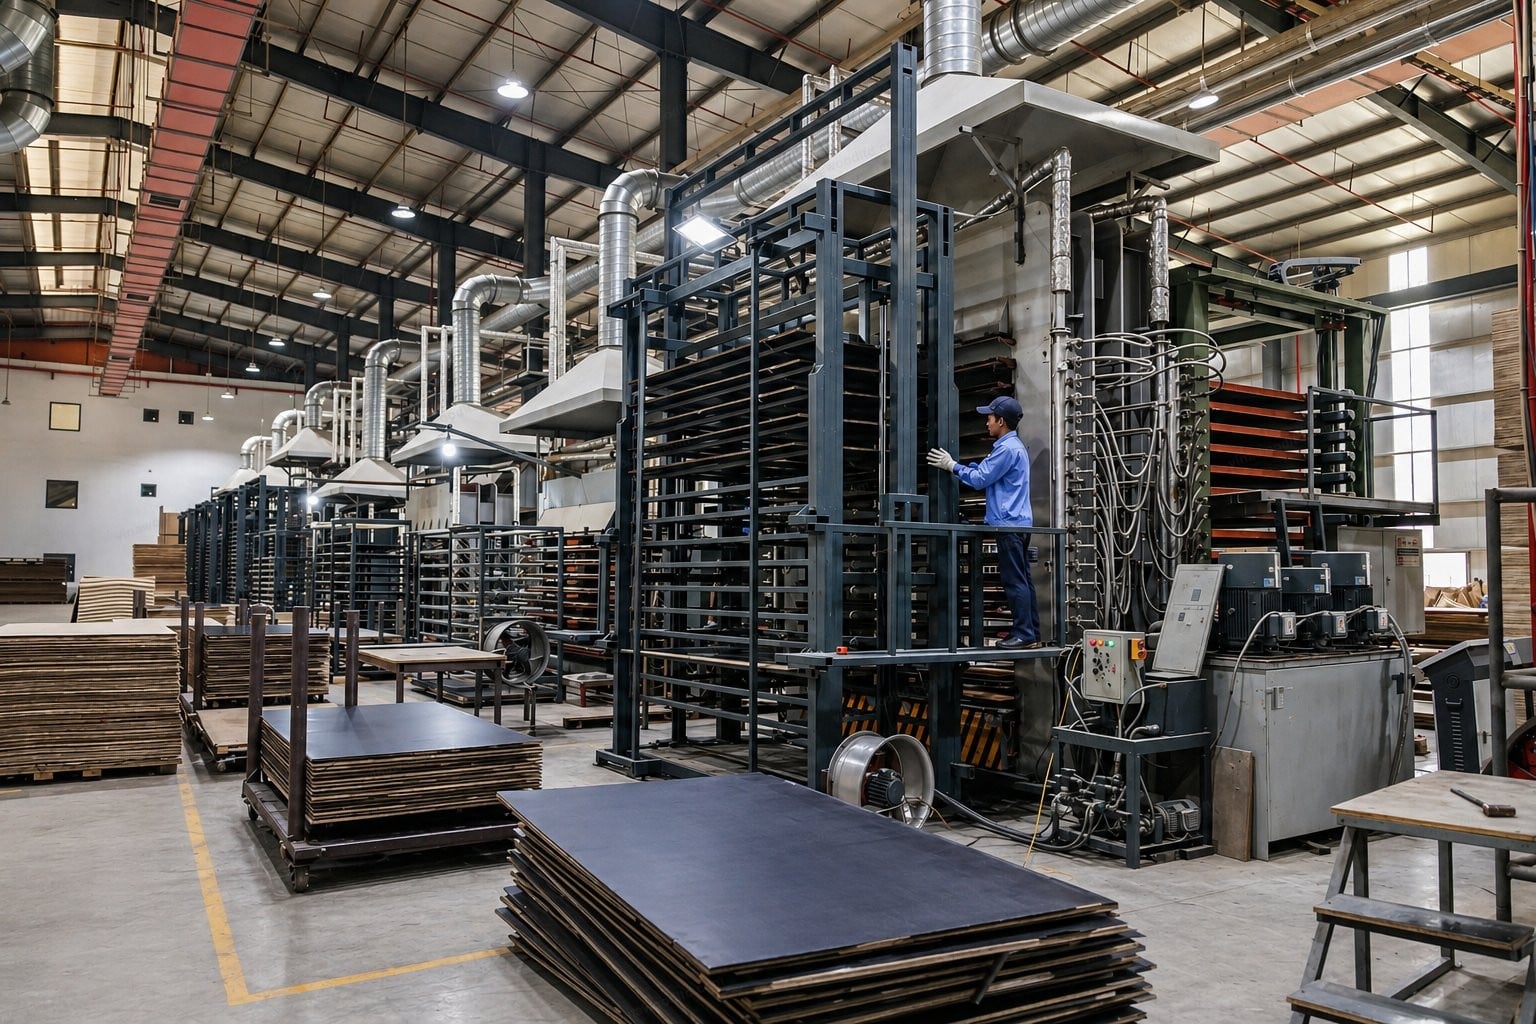
APA-style BB/OES and BB plyform are the sanded North American baseline: exterior glue, oiled before use, wood grain printed onto the concrete. Fine for buried work, but we don't make that SKU and it shouldn't be compared like-for-like with an overlaid panel. Marine plywood isn't a forming overlay either. Its grain prints and it has no formwork reuse rating, so for boats or wet interiors start with film-faced plywood vs marine plywood.
What are the sizes of form ply?
North American gangs are still built on 1220 × 2440 mm (4 × 8 ft). Metric markets add 1250 × 2500 mm as a stock film-faced module, and a lot of European wall frames assume it. Mix the two on one wall and you get a lip at every joint, so order what the frames were designed around.
Eighteen millimetres (3/4 in) is the workhorse, with 12 mm (1/2 in), 15 mm (5/8 in) and 21 mm common too. Pour pressure and stud or joist spacing set the thickness, not the catalogue photo. Tolerance counts just as much, because a slightly fat sheet beside a slightly thin one becomes a visible step, so film-faced lots should be checked against EN 315.
Applications of plywood formwork
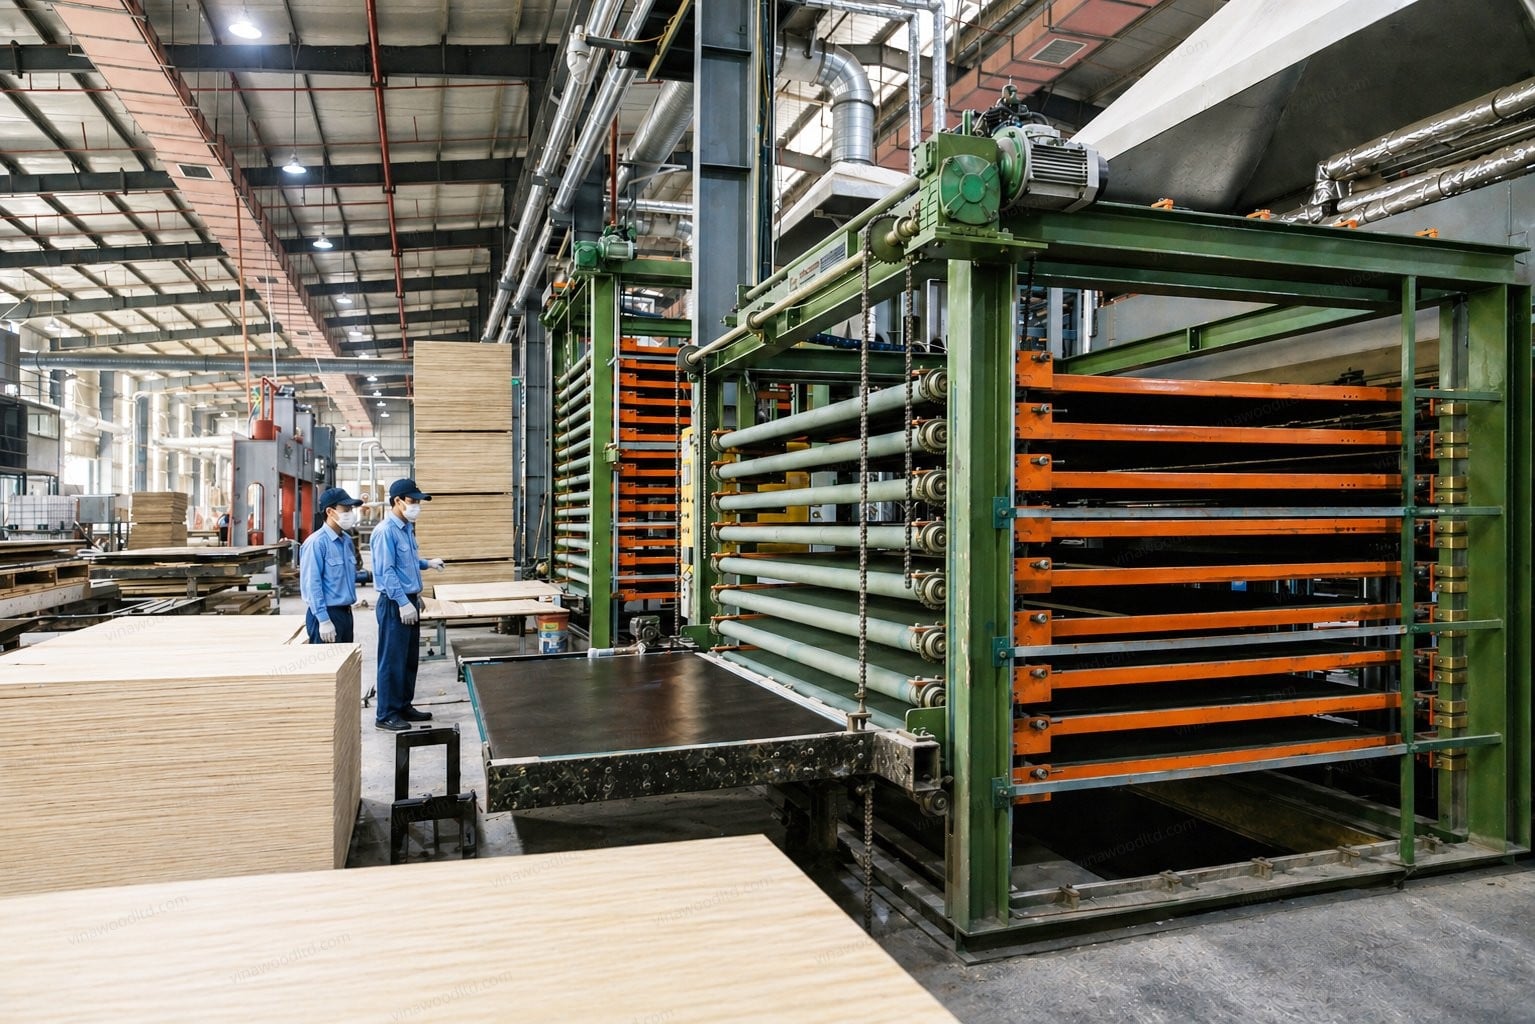
On walls and columns the plywood is a thin skin on one side of a metal gang; from the walkway you see walers and strongbacks, while the film faces the pour. Slabs flip that. The sheet lies on timber joists over steel props and makes up just the top 18 mm of a structure that's mostly open air. Tunnels and bridge piers often call for a Class 3 film plus a crane plan, and high-rise cores, cycling one gang floor after floor, are where an "up to 20" panel pays back its premium.
A deck and a wall look alike in photos and behave nothing alike. Span, deflection and support change, so a panel chosen for a wall form shouldn't be copied onto a tableform deck without a check. Slab layout is on slab formwork plywood.
Where to buy forming plywood
Vinawood is a factory-direct plywood manufacturer in Vietnam, not a retail store, and our grades aren't stocked in big-box lumber aisles. Container programmes go through the RFQ form or the quotation form; we don't publish sheet prices. For ready stock, Vinawood keeps distribution warehouses in Toronto, Vancouver, Calgary, Montreal, Miami, Houston and Baltimore that supply local distributors, so a North American yard enquiry can often be filled from inventory nearer the job. Vessel schedules and inspection slots still move lead times around. Don't plan a first pour off a blog post.
We've made plywood since 1992 and ship about 5,000 containers a year to 55+ countries. Each lot passes a twelve-step process, peeling and drying through pressing, overlay and edge sealing, and every sheet is inspected before packing under ISO 9001. A packing list, mill test report and Declaration of Performance travel with it. Without those papers, the overlay colour says very little about what's underneath. Origin comparisons are on plywood manufacturers Vietnam, and Canadian distributors can find yard language in the Canada film-faced suppliers note.
How to choose the right formwork plywood
Describe the job in the mill's four fields and the choice gets much easier. The drawings' finish picks the overlay family: HDO for gloss, MatteFace for matte, film-faced for general reusable work. Site wetness and cycle count set the bond class, remembering that only Pro Form, Pro Form Lite, HDO Standard and HDO Premium are Class 3 on our list. Frames and destination market take care of size and emission class.
For reuse, divide the forming area by one sheet, then by the pours in the programme; that number usually rules a few grades out on the spot, and beyond about ten cycles bare plyform stops making sense. How close you get to the ceiling is a site habit. Release agent on every pour, plastic scrapers instead of steel bars, sheets stored face to face on bearers under cover.
Request mill specs for your next pour
Put overlay, bond class, size and emission class on the RFQ, and attach the pour programme if you have one. Cores are plantation-grown Acacia or Eucalyptus, Hevea on some lots, and every lot ships with its test report and DoP. Send it through the RFQ or the quotation form; we'll reply with the grade that fits your finish and cycle count, not simply the lowest-priced sheet on the list.
Category
guides